Manufacturing processes for engineering materials and how to choose them
What the term covers
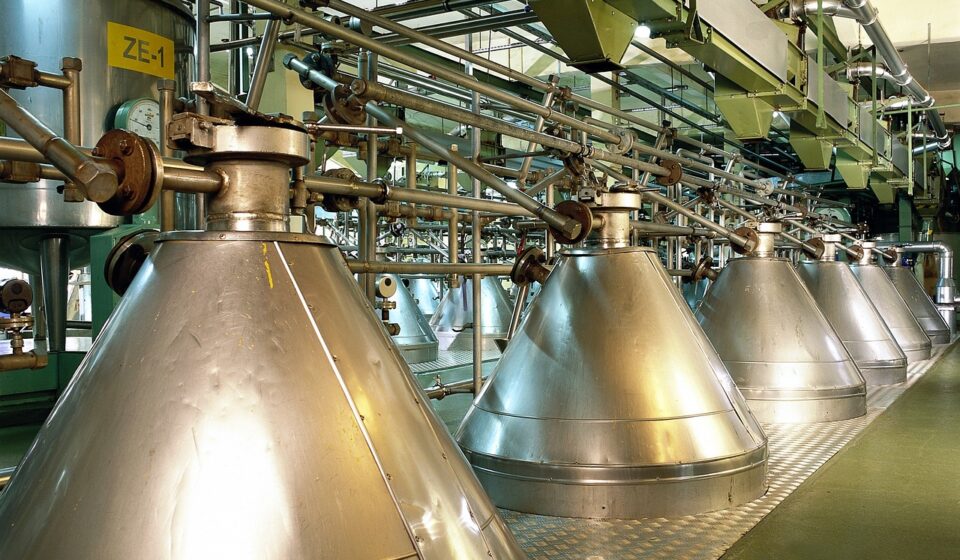
Manufacturing processes for engineering materials are the methods used to turn raw stock, powders, melts, sheets, fibers, or other feedstock into components with a specified shape, tolerance, surface condition, and set of mechanical properties. The term usually covers metals and alloys, polymers, ceramics, glasses, and composites. A sound process choice is not limited to whether a route can form the geometry. It must also consider whether the material can tolerate the thermal, mechanical, and chemical conditions of the process, whether the finished part can meet strength and reliability requirements, and whether the route fits the expected production volume and cost.
For more process-focused articles, see the manufacturing processes section. In practice, the aim is to align material behavior, part geometry, production scale, and quality controls before tooling or supplier decisions create avoidable risk.
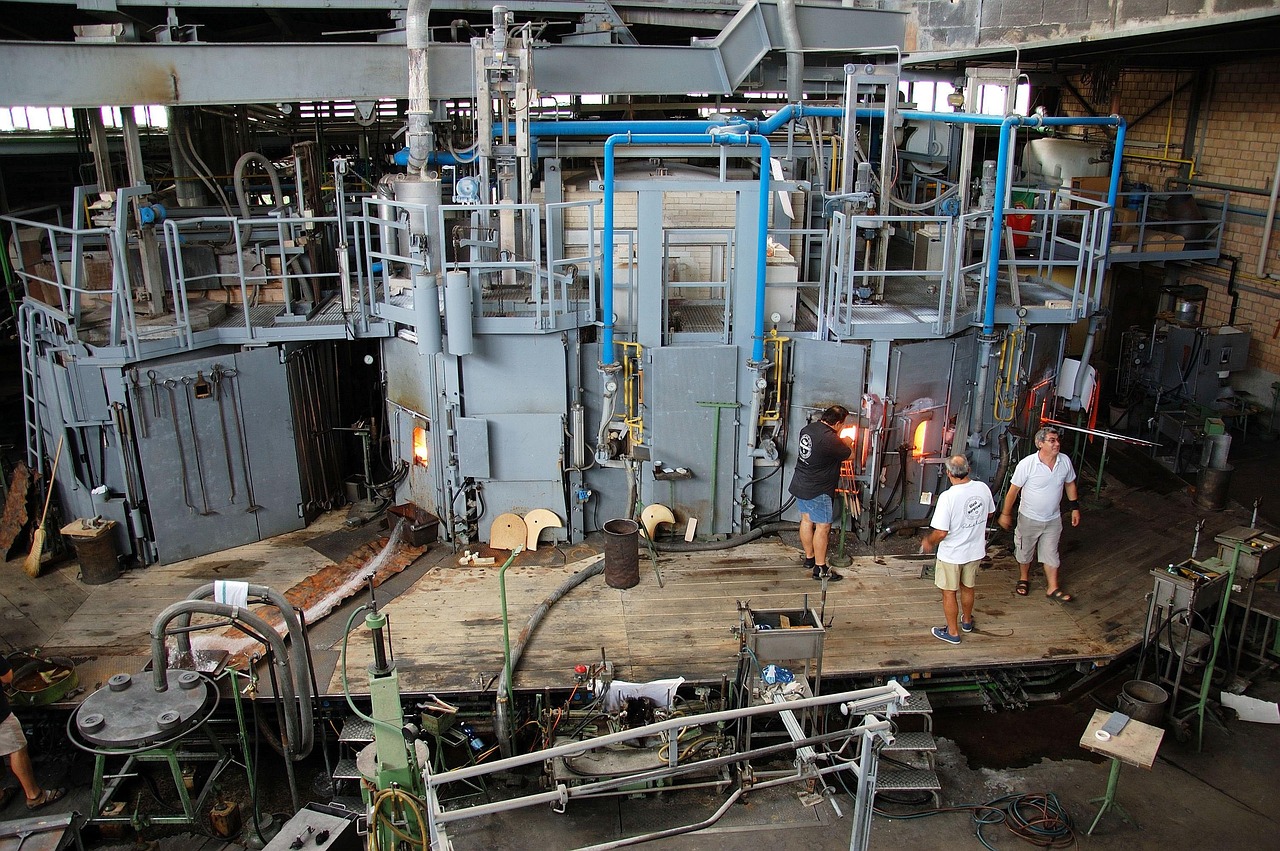
Major process families used in engineering materials
Industry references such as the ASM Handbook group manufacturing methods into broad families, including casting, deformation processing, powder processing, machining, joining, polymer processing, ceramic and glass processing, and composite manufacturing. U.S. Department of Energy training materials also use a practical hierarchy: primary shaping processes, secondary processes, and assembly or test processes. Together, these views help engineers compare full process routes instead of treating each operation as a separate decision.
Primary shaping processes
Primary shaping creates the main form of a part. For metals, this may include sand casting, die casting, investment casting, forging, rolling, extrusion, sheet forming, or powder metallurgy. For polymers, it often means injection molding, extrusion, blow molding, compression molding, thermoforming, or rotational molding. For ceramics, common routes include powder compaction followed by sintering, slip casting, hot pressing, and glass forming. For composites, primary shaping may involve hand lay-up, resin transfer molding, filament winding, pultrusion, compression molding, or autoclave curing.
Additive manufacturing is also a primary shaping route when the printed geometry is close to the final form. It is especially useful when a design benefits from internal channels, lattice structures, low tooling investment, or rapid design iteration. For load-bearing applications, however, it usually still requires qualification, inspection, and post-processing before it can replace conventional production routes.
Secondary processes and finishing
Secondary operations refine dimensions, properties, and surfaces. Machining, grinding, drilling, laser cutting, electrical discharge machining, and waterjet cutting remove material to achieve tighter tolerances or create features that are difficult to form directly. Heat treatment can alter hardness, ductility, residual stress, or microstructure. Surface treatments such as plating, anodizing, painting, polishing, coating, and shot peening change corrosion resistance, appearance, friction, fatigue performance, or wear behavior.
Joining, assembly, and inspection
Few engineered products are made with a single process. Welding, brazing, soldering, adhesive bonding, riveting, bolting, and mechanical assembly connect parts into usable systems. Inspection then verifies dimensions, material condition, surface integrity, and functional performance. A process route is therefore a chain. A strong casting process may still be a poor production choice if machining stock is insufficient, weld distortion is uncontrolled, or inspection cannot detect a critical internal defect.
Material process compatibility by material class
Material compatibility is the first filter in process selection. The table below summarizes common routes and typical constraints. It is not a substitute for design allowables, supplier capability data, or applicable standards, but it helps narrow the search before detailed engineering work begins.
| Material class | Common process routes | Why these routes are used | Typical limitations to check |
|---|---|---|---|
| Metals and alloys | Casting, forging, rolling, extrusion, sheet forming, powder metallurgy, machining, welding, additive manufacturing | Metals can often be melted, plastically deformed, joined, and heat treated to adjust strength and toughness | Shrinkage, porosity, residual stress, tool wear, heat-affected zones, distortion, grain structure, and corrosion behavior |
| Polymers | Injection molding, extrusion, blow molding, compression molding, thermoforming, material extrusion printing, vat photopolymerization | Thermoplastics can be softened and reshaped; thermosets can be cured into stable forms; tooling supports high-volume production | Shrinkage, warpage, moisture sensitivity, thermal limits, weld lines, creep, UV exposure, and recycling constraints |
| Ceramics and glasses | Powder pressing and sintering, slip casting, hot pressing, glass forming, grinding, polishing, additive routes for selected materials | Powder and thermal routes suit materials that are hard, wear resistant, heat resistant, or chemically stable | Brittleness, sintering shrinkage, cracking, machining difficulty, density variation, and inspection of internal flaws |
| Composites | Lay-up, autoclave curing, filament winding, pultrusion, resin transfer molding, compression molding, adhesive bonding, trimming | Fibers and matrices can be oriented to provide high stiffness or strength in selected directions | Anisotropy, delamination, voids, fiber alignment, cure control, edge damage, moisture ingress, and repair complexity |
How manufacturing changes material properties
Engineering materials do not retain identical properties across all processing routes. Manufacturing can change grain size, phase distribution, porosity, residual stress, fiber orientation, crystallinity, surface roughness, hardness, and defect populations. For that reason, process selection should be considered as part of material selection, not as a separate step after the material has already been chosen.
Thermal history
Casting, welding, heat treatment, sintering, polymer molding, and many additive processes depend on controlled heating and cooling. Cooling rate can influence metal microstructure, polymer crystallinity, ceramic density, and residual stress. A route that appears economical can become unreliable if thermal gradients cause distortion, cracking, or property variation from one area of the part to another.
Deformation and work hardening
Forging, rolling, extrusion, drawing, stamping, and bending reshape material through plastic deformation. These processes can improve strength, refine grain structure, and align material flow with load paths. They can also introduce springback, residual stress, cracks, or anisotropy if the alloy, temperature, lubrication, die design, and forming sequence are not controlled.
Surface integrity
Machining, grinding, polishing, coating, and peening affect more than appearance. Surface roughness can influence fatigue, sealing, friction, wear, and corrosion. In high-performance components, a small surface defect or tensile residual stress near the surface may matter more than the average bulk strength of the material. See also: cnc and robotics.
Additive manufacturing adds options but not shortcuts
ISO/ASTM 52900:2021 defines additive manufacturing vocabulary and is commonly associated with seven process categories: binder jetting, directed energy deposition, material extrusion, material jetting, powder bed fusion, sheet lamination, and vat photopolymerization. These categories are useful because they describe how material is added, joined, cured, or fused, rather than relying on brand names or machine-specific labels.
NIST has emphasized that measurement science, standards, benchmark testing, and reference materials are important as additive manufacturing matures. That point is important for engineering materials because a printed part is not defined only by its nominal material grade. Powder condition, feedstock traceability, build orientation, layer strategy, atmosphere control, machine calibration, post-build heat treatment, surface finishing, and inspection can all influence performance.
Additive manufacturing can reduce tooling, consolidate assemblies, and enable geometries that are impractical with machining or casting. It may also introduce rough surfaces, anisotropic properties, internal defects, support-removal constraints, slower cycle times, and more demanding qualification requirements. In many industrial applications, the strongest route is hybrid: additive manufacturing for shape complexity, machining for interfaces, heat treatment for properties, and inspection for risk control.
A practical workflow for choosing a process
- Define the service requirements. Start with loads, temperature, environment, wear, corrosion, fatigue life, electrical or thermal behavior, regulatory requirements, and expected failure modes.
- Shortlist compatible materials. Separate material needs from manufacturing assumptions. A material that performs well in service may still be difficult or expensive to shape.
- Identify the basic shape route. Decide whether the part is best approached as a casting, molding, forging, sheet component, machined billet, powder part, composite lay-up, or additive build.
- Check volume and tooling economics. High-volume polymer parts may justify injection molding tools, while low-volume or evolving designs may favor machining, additive manufacturing, or soft tooling.
- Map secondary operations. Include machining allowances, heat treatment, surface finishing, joining, cleaning, and inspection before comparing cost or lead time.
- Evaluate capability and tolerances. Confirm whether the process can hold the required dimensions, surface finish, wall thickness, holes, threads, flatness, and repeatability.
- Assess quality risks. Look for process-specific risks such as casting porosity, weld defects, polymer warpage, ceramic cracking, composite voids, or additive lack of fusion.
- Document controls. A stable route should specify material grade, process parameters, acceptance criteria, inspection methods, and change-control requirements.
Process comparison examples
The same material can often be manufactured in several ways. The best route depends on the part’s function, geometry, production volume, and risk tolerance.
| Part requirement | Likely process route | Reasoning |
|---|---|---|
| Complex metal housing with internal cavities | Casting followed by machining and inspection | Casting forms the near-net cavity geometry; machining controls sealing faces, holes, and datums |
| High-strength shaft or connecting component | Forging, heat treatment, and finish machining | Deformation can improve material flow and strength; machining finishes bearing and assembly surfaces |
| High-volume polymer enclosure | Injection molding with secondary finishing if needed | Tooling cost can be justified by repeatable cycle time, integrated features, and low part cost at scale |
| Lightweight composite tube | Filament winding or pultrusion | Fiber orientation can be aligned with torsion, pressure, or axial load requirements |
| Low-volume metal part with internal channels | Powder bed fusion, heat treatment, machining, and nondestructive evaluation | Additive manufacturing enables geometry that may be difficult to machine, but post-processing and inspection remain central |
Common mistakes in process selection
- Choosing the process too late. If the design is completed before process planning, avoidable features may force costly tooling, excessive machining, or weak joints.
- Comparing only the primary operation. A near-net process may appear cheaper until heat treatment, finishing, inspection, scrap, and qualification are included.
- Ignoring material variability. Nominally identical grades can perform differently if processing changes microstructure, porosity, fiber orientation, or residual stress.
- Overvaluing novelty. Advanced processes are valuable when they solve a real constraint. They are not automatically better than casting, forming, molding, or machining.
- Underestimating inspection. A process is only production-ready when critical defects can be prevented, detected, or shown to be irrelevant to performance.
Frequently asked questions
What are the main manufacturing processes for engineering materials?
The main families include casting, forming, molding, powder processing, machining, joining, heat treatment, surface finishing, composite processing, ceramic processing, and additive manufacturing. Most real production routes combine more than one family.
How do engineers choose between casting, forging, machining, and additive manufacturing?
They compare material compatibility, geometry, production volume, mechanical requirements, tolerances, surface finish, tooling cost, lead time, and inspection risk. Casting often suits complex metal shapes, forging suits high-strength load paths, machining suits precision features and lower-volume parts, and additive manufacturing suits complex or low-tooling geometries.
Why is material selection connected to process selection?
Manufacturing changes material properties. Heat, deformation, cooling rate, curing, sintering, machining, and joining can alter microstructure, residual stress, surface condition, defect levels, and strength. A material that is excellent in a datasheet may fail to meet requirements if processed incorrectly.
Is additive manufacturing a replacement for conventional processes?
Not generally. Additive manufacturing expands the design and production toolkit, especially for complex, low-volume, or highly customized parts. Conventional processes remain efficient for many high-volume, high-precision, and well-qualified applications. Hybrid routes are often the most practical choice.