Engineering & machining precision in modern manufacturing
What engineering & machining precision really means
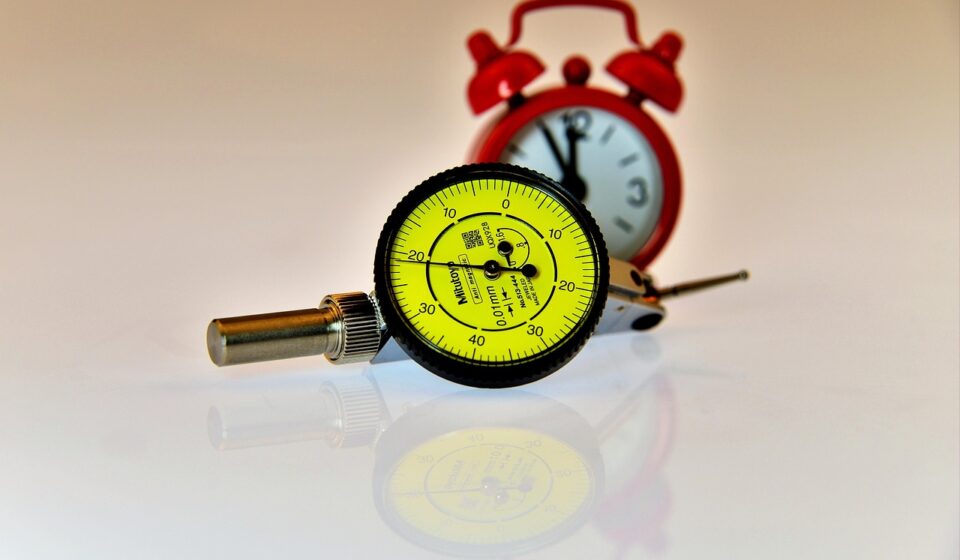
Engineering & machining precision is the controlled ability to define, produce, and verify part features so they perform as intended in an assembly. On the engineering side, it starts with the drawing or model, material selection, datum scheme, tolerance budget, and inspection requirement. On the machining side, it is the shop-floor ability to meet those requirements repeatedly through capable equipment, tooling, workholding, thermal control, cutting parameters, and measurement methods.
Precision does not mean making every dimension as tight as possible. It means controlling the features that affect fit, motion, sealing, alignment, safety, or service life, and proving that the result can be repeated. This distinction matters because unnecessary tight tolerances add cost, slow production, increase scrap risk, and may still leave the functional surfaces under-controlled.
Precision starts with a shared technical language
Modern precision manufacturing depends on standards because a tolerance is useful only when designers, machinists, inspectors, and suppliers interpret it in the same way. In the United States, ASME Y14.5 is widely used for geometric dimensioning and tolerancing, often called GD&T. The 2018 edition was reaffirmed in 2024 by ASME, and it remains a common reference for specifying form, orientation, location, profile, runout, datums, and related drawing rules. Internationally, the ISO geometrical product specifications system provides a broader framework for defining and verifying geometry, including size, form, fits, surface texture, and measurement equipment.
For machining teams, the practical requirement is clear: the drawing or model should state the governing standard and edition when this is required by contract or quality procedure. Mixing ASME and ISO conventions without clarification can lead to disputes over datums, size interpretation, envelope requirements, and inspection decisions.
| Reference area | What it controls | Why it matters for precision machining |
|---|---|---|
| ASME Y14.5 GD&T | Symbols, rules, datums, tolerance zones, and interpretation | Reduces ambiguity between design, machining, and inspection teams |
| ISO GPS system | International rules for geometrical specification and verification | Supports consistent interpretation across global supply chains |
| ISO 286 limits and fits | Standardized tolerance classes for holes and shafts | Helps define clearance, transition, and interference fit behavior |
| ISO 14978 | General concepts and requirements for GPS measuring equipment | Connects measurement tools with the specifications they verify |
| ISO 25178 surface texture | Areal surface texture indication and parameters | Improves communication when 3D surface behavior matters |
How design intent becomes a machinable tolerance
A precise part starts with functional thinking. A bore that locates a bearing, a sealing face, a sliding guide, and a cosmetic cover surface should not be controlled with the same tolerance logic. The bearing bore may require size, cylindricity, coaxiality, and surface texture control. The sealing face may require flatness and roughness control. The cover surface may need only a general profile or visual requirement. Treating all features as equally critical wastes machining effort and can still miss the characteristic that actually drives product performance.
Define datums around function, not convenience
Datums should represent how the part is assembled, located, or used. A datum chosen only because it is easy to touch with a probe can create a false sense of precision. If a part mounts on one face and locates through two pins, those functional contacts usually deserve priority in the datum reference frame. Machining fixtures and inspection fixtures can then be planned around the same functional relationship.
Use tolerance budgets before releasing the drawing
Precision should be allocated, not guessed. A tolerance stack-up shows how individual feature variation affects final assembly clearance, alignment, preload, sealing, or motion. If the stack-up shows that one feature drives most of the risk, the designer can tighten that feature while keeping noncritical dimensions practical. If the stack-up shows excessive sensitivity, the better answer may be a design change rather than a more expensive machining process.
For more related manufacturing analysis, visit the precision engineering section.
Process variables that determine machining precision
CNC equipment is essential, but the machine alone does not guarantee precision. Repeatable results depend on the whole process chain. A machine tool may be geometrically accurate after calibration, yet a part can still drift out of tolerance because of tool wear, heat growth, unstable clamping, residual stress, or an inspection method that does not match the specification.
- Machine condition: axis geometry, spindle health, backlash control, servo behavior, volumetric accuracy, and maintenance history influence repeatability.
- Thermal stability: machine warm-up, coolant temperature, shop temperature, and heat from cutting can shift dimensions during a run.
- Workholding: clamping force, locator wear, fixture rigidity, and part distortion can change the final geometry after unclamping.
- Tooling: insert wear, tool runout, holder rigidity, tool length offsets, and cutter deflection directly affect size and surface finish.
- Material behavior: hardness variation, cast or forged structure, residual stress, and heat treatment can change how the part responds to machining.
- Machining sequence: roughing, stress relief, semi-finishing, finishing, and inspection timing should be planned together for critical parts.
High precision work often uses a staged approach: remove bulk material, allow the part to stabilize when necessary, re-locate on functional datums, finish critical features, and verify them under controlled conditions. This is slower than treating machining as a single toolpath problem, but it is more reliable when tolerances are tight or geometry is complex.
Measurement precision is part of the manufacturing system
A part cannot be managed to a tolerance unless the measurement system can distinguish good parts from bad parts. Guidance from NIST on measurement process characterization emphasizes calibration, repeatability, reproducibility, stability, bias, linearity, hysteresis, drift, and uncertainty. In production terms, the measuring method must be suitable for the tolerance, feature geometry, operator environment, and the decision being made.
Gauge repeatability and reproducibility studies can be useful, but they must represent the real measurement process. A study performed in ideal conditions may not reflect the uncertainty of measurements taken beside a machine, on warm parts, by different operators, or with changed fixtures. NIST also notes that uncertainty estimates based on gauge studies can become unreliable if the measurement process changes over time.
| Inspection evidence | What it shows | Limit to watch |
|---|---|---|
| Calibration record | The instrument is traceable and within its calibration interval | Calibration alone does not prove the method is suitable for the tolerance |
| CMM report | Measured geometry against a defined program and setup | Results depend on datum simulation, probe strategy, temperature, and software settings |
| Gauge R&R study | Repeatability and reproducibility of a measurement method | The study must match real operators, parts, fixtures, and environment |
| Surface measurement | Texture or roughness characteristics of functional surfaces | Parameter, filter, direction, and instrument type must match the requirement |
| Process capability data | How a stable process performs over a sample period | Capability numbers are weak if the process is drifting or the sample is not representative |
A practical workflow for precision planning
Precision improves when engineering, machining, and inspection decisions are made together rather than passed from one team to the next. The following workflow can be applied to prototypes, pilot runs, and production parts. See also: cnc and robotics.
- Identify functional features. Separate assembly, sealing, bearing, motion, alignment, and cosmetic requirements.
- Choose the governing specification system. State whether the drawing follows ASME Y14.5, ISO GPS, customer standards, or a defined contract requirement.
- Build a tolerance budget. Connect feature variation to assembly performance before selecting arbitrary decimals.
- Review manufacturability. Check whether tolerances match the material, geometry, access, fixture concept, and available process.
- Plan the machining sequence. Decide where roughing, stress relief, datum creation, finishing, deburring, cleaning, and inspection occur.
- Define inspection at the same time. Confirm the CMM program, gauges, surface measurement method, environmental controls, and reporting format.
- Run a controlled first article. Use early parts to validate datum interpretation, toolpath strategy, offsets, and inspection correlation.
- Monitor the process. Track wear, temperature, offsets, measurement trends, and nonconformance patterns instead of relying only on final inspection.
This workflow does not guarantee perfect parts. It does reduce avoidable disagreement because each key decision is tied to function, process capability, and measurement evidence.
Common precision failures and how to prevent them
Many precision problems are not caused by poor machining skill. They come from unclear requirements, mismatched measurement methods, or decisions made too late in the project. The table below summarizes frequent failure modes in engineering and machining precision work.
| Failure mode | Typical cause | Prevention |
|---|---|---|
| Over-tolerancing noncritical features | Using tight decimals as a substitute for functional analysis | Classify features by function and assign tolerance only where it affects performance |
| Datum disagreement | Design, fixture, and inspection teams simulate the part differently | Review datum targets, fixturing, and inspection setup before release |
| Good part fails inspection | CMM method does not match the drawing interpretation | Align the inspection plan with GD&T or ISO GPS rules before production |
| Dimension changes after unclamping | Part distortion from clamping force or residual stress | Use balanced machining, staged operations, stress relief, and functional re-location |
| Surface passes roughness but fails function | Wrong parameter or measurement direction for sealing, sliding, or fatigue behavior | Specify the surface parameter and measurement method that match the function |
| Capability declines during production | Tool wear, temperature drift, fixture wear, or material variation | Use process monitoring and defined reaction plans, not final inspection alone |
Digital tools help, but they do not replace engineering judgment
Model-based definition, CMM software, in-process probing, tool monitoring, and machine error compensation can make precision manufacturing more consistent. They reduce transcription errors, support faster feedback, and help connect design data with inspection data. However, digital tools still depend on correct datums, realistic tolerances, controlled processes, and validated measurement methods. A perfect 3D model with unclear functional intent can still create expensive ambiguity. Likewise, an automated inspection report is only as reliable as the measurement strategy behind it.
The strongest precision programs use digital information as a controlled thread, not as a substitute for communication. Revision control, drawing notes, model authority, inspection plans, and supplier requirements should tell the same story. When they do, engineering & machining precision becomes a managed system rather than a last-minute quality check.
Frequently asked questions
Is tighter tolerance always better?
No. A tighter tolerance is useful only when it protects function, safety, reliability, interchangeability, or assembly performance. Unnecessary tight tolerances can increase cost, inspection time, scrap, and supplier risk without improving the product.
How are accuracy and precision different in machining?
Accuracy describes closeness to the intended value. Precision describes repeatability or consistency. A process can be precise but offset from nominal, or accurate on one part but not repeatable across production. High-quality machining requires both, plus a measurement system that can verify them.
Which standard should a drawing use, ASME Y14.5 or ISO GPS?
The answer depends on the customer, region, contract, and supply chain. ASME Y14.5 is common in many U.S.-based industries, while ISO GPS is widely used internationally. The important step is to state the applicable standard clearly and avoid mixing interpretation rules without explanation.
Can CMM inspection prove a process is capable?
A CMM report can show measured results for inspected parts, but it does not by itself prove long-term process capability. Capability requires representative sampling, stable process conditions, suitable measurement uncertainty, and evidence that variation remains controlled over time.
What should be checked before quoting a precision machining job?
Review the material, critical features, tolerance standard, datum scheme, surface requirements, inspection requirements, batch quantity, heat treatment, post-processing, documentation needs, and whether the tolerance can be measured reliably. Quoting precision without reviewing the measurement requirement is a common source of risk.