Bespoke precision engineering for complex, high-tolerance manufacturing
What bespoke precision engineering means in practice
Bespoke precision engineering covers the development and manufacture of custom mechanical parts, assemblies or tooling when a catalogue component, standard drawing or routine machining route is not enough. It brings together design interpretation, material selection, precision machining, measurement planning and quality control around one specific requirement. In high-tolerance manufacturing, the value is not just tighter dimensions. It is knowing which features matter, how they will be produced, how they will be inspected and how production risk will be controlled. For readers comparing methods across precision engineering, the practical question is whether a bespoke route creates a clearer path from function to verified part.
The word bespoke is sometimes used loosely in manufacturing marketing. In a serious engineering context, it should mean that the production plan is shaped by the application, rather than forcing the application into an existing part family. That may involve custom fixtures, non-standard materials, a tailored inspection plan, special surface finish requirements, controlled documentation or close collaboration between design and manufacturing teams before release.
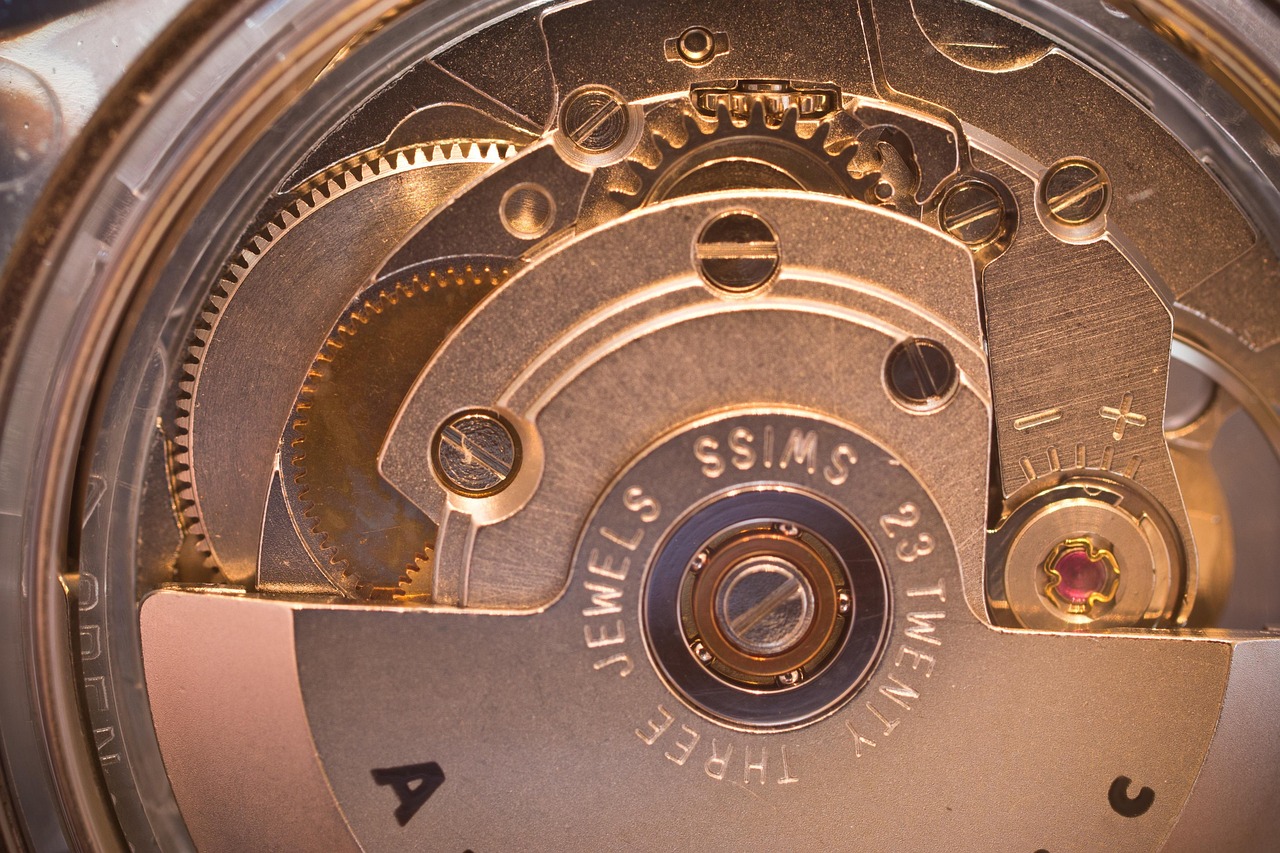
This approach is most useful where failure would be costly, where geometry is difficult to inspect after assembly, where interchangeability matters, or where a part must perform reliably under thermal, load, wear or cleanliness constraints. It can support one-off prototypes, development batches and repeat production, but each case needs a different balance between speed, cost and process control.
When a bespoke route makes sense
Not every engineered part needs bespoke precision engineering. If the requirement can be met by a standard fastener, bearing, shaft, bracket or catalogue fitting, a custom route may add cost without adding value. The case becomes stronger when the part has a direct influence on performance, safety, service life, assembly accuracy or downstream manufacturing efficiency.
Common triggers include unusual geometry, very close positional relationships between features, difficult materials, demanding flatness or concentricity requirements, a need for controlled surface texture, or interface dimensions that must match legacy equipment. A bespoke route may also be appropriate when the part is part of a larger system and the better engineering decision is to optimize the component around the system rather than buy around the component.
- Functional criticality: the part controls motion, sealing, alignment, load transfer, heat flow or repeatability.
- Limited standard options: available components are close, but not close enough for the required fit, envelope or duty cycle.
- Inspection complexity: quality cannot be confirmed by a simple caliper check and needs a planned measurement method.
- Material or environment constraints: corrosion, temperature, vibration, contamination or wear changes the design decision.
- Lifecycle value: a better custom component can reduce assembly time, scrap, adjustment work or field replacement.
The key test is whether the extra engineering effort reduces overall risk. A more expensive part can still be the economical option if it prevents repeated rework, unstable assembly, premature wear or unclear acceptance criteria.
From requirement to verified component
A successful bespoke precision engineering project starts before the first cutting tool touches the workpiece. The early work is about translating functional intent into manufacturable and inspectable requirements. Many cost and quality problems begin when a drawing asks for tight tolerances everywhere, omits datum logic, or defines a surface finish without explaining which function it protects.
Define the function first
The first step is to identify what the part must do. Does it locate another component, transmit torque, maintain a seal, carry a bearing, guide a sliding element or hold an optical or sensor position? Function should drive the choice of critical features. Without this step, tolerances can become either too loose for performance or unnecessarily tight for manufacturing.
Translate intent into tolerances
Once the function is clear, engineering teams can decide which dimensions, geometrical controls and surface requirements are truly critical. For example, a bore may need diameter control, roundness control and positional control relative to a mounting face, while an external profile may only need a general tolerance. This separation helps suppliers focus process capability and inspection effort where it matters most.
Plan inspection before production
Inspection should not be treated as an afterthought. Features that are easy to model can be difficult to measure, especially after heat treatment, coating, assembly or access restrictions. A robust plan defines the inspection equipment, datum setup, sampling method, records required and acceptance rules before production begins. This is particularly important when coordinate measuring machines, optical systems, surface measurement equipment or custom gauges are involved.
The best bespoke projects create a feedback loop between design, manufacturing and metrology. If a tolerance is technically possible but difficult to measure repeatedly, the team should either justify it, adjust the design or define a more reliable verification route.
Standards, tolerances and inspection language
Precision engineering depends on shared language. A drawing or model can only control quality if the designer, manufacturer and inspector interpret it in the same way. Public standards do not replace engineering judgement, but they reduce ambiguity when used correctly and when the exact edition is specified.
| Reference | Role in precision work | Why it matters in bespoke projects |
|---|---|---|
| ISO 1101:2017 | Defines a symbol language and interpretation rules for geometrical tolerancing of workpieces. ISO records show this edition was confirmed in 2022. | Supports clear control of form, orientation, location and run-out when simple plus-minus dimensions are not enough. |
| ASME Y14.5-2018, reaffirmed 2024 | Provides rules, symbols, definitions and practices for geometric dimensioning and tolerancing. | Helps design, machining and inspection teams communicate design intent across drawings, digital models and related documents. |
| ISO 9001 quality management requirements | Defines requirements for a quality management system rather than a specific machining method. | Useful as a procurement and process framework, but it does not by itself prove that a supplier can hold a particular tolerance. |
| NIST work on smart manufacturing and digital thread concepts | Addresses data integration, manufacturing information flow and model-based approaches. | Reinforces the importance of connecting design data, process data and quality records instead of treating them as isolated documents. |
One common mistake is to specify a standard without defining how it applies to the project. Another is to copy tolerances from an old drawing without checking whether they still support the current function. For bespoke precision engineering, the more useful approach is to combine a recognized standard with a clear drawing, a controlled model where applicable, and an inspection plan that matches the risk level.
General tolerances also need care. They can be appropriate for non-critical features, but they should not hide important functional requirements. If a mounting face, bore, slot or sealing land is critical, it deserves explicit control and a verification method.
Process choices that shape cost, quality and lead time
Bespoke precision engineering is not a single manufacturing process. It may involve CNC milling, turning, grinding, EDM, honing, lapping, laser processes, additive manufacturing, fabrication, heat treatment, coating, cleaning and assembly. The right route depends on geometry, material behavior, tolerance stack-up and inspection access. See also: cnc and robotics.
Material selection is often where engineering compromise becomes visible. A high-strength alloy may meet load requirements but create machining difficulty, tool wear, distortion risk or heat treatment movement. Stainless steels can improve corrosion resistance but vary widely in machinability and finishing behavior. Aluminium alloys can support lightweight designs, but surface protection, thread durability and thermal expansion may become design issues. Plastics and composites can solve weight, friction or electrical problems, but moisture absorption, creep and temperature limits may matter.
Process sequencing can be just as important as process selection. If a part needs both heat treatment and tight final geometry, the plan may require rough machining, stress relief, heat treatment and finish machining. If a coating adds measurable thickness, the coating must be considered in the drawing and inspection plan. If the part will be cleaned for a sensitive assembly, burr control, trapped contamination and packaging may be part of the engineering requirement rather than a cosmetic preference.
Lead time is affected by more than machining hours. Bespoke work often requires drawing clarification, fixture design, programming, material procurement, first-article inspection and corrective action if the first route does not meet the requirement. Compressing this preparation may appear to save time, but it often transfers risk to inspection or assembly.
How buyers can reduce risk when specifying a project
Buyers and project engineers can improve outcomes by making requirements precise without making them unnecessarily restrictive. A supplier cannot act on vague phrases such as high quality or tight tolerance. It needs a controlled drawing or model, material specification, critical features, expected quantities, inspection expectations and any documentation requirements.
- State the application context: explain what the component does and which interfaces are critical.
- Identify critical-to-function features: separate essential tolerances from general manufacturing limits.
- Specify the applicable standard and edition: avoid assuming that all parties use the same tolerancing interpretation.
- Define inspection records: clarify whether dimensional reports, material certificates, surface finish data or first-article inspection are required.
- Discuss manufacturing constraints early: ask whether a small design change could reduce cost, improve yield or simplify measurement.
- Control revisions: make sure drawing, model, purchase order and inspection documents refer to the same revision.
For recurring parts, buyers should also ask how knowledge from the first batch will be captured. Tooling notes, measurement lessons, nonconformance history and process adjustments can make the second and third production runs more stable. In that sense, bespoke precision engineering is not only about producing one difficult part; it is about creating a repeatable path for a requirement that standard manufacturing cannot safely absorb.
The commercial conversation should also reflect uncertainty. If a part is experimental, it may be better to order a development batch and review inspection results before committing to a larger quantity. If the requirement is mature, the focus can shift to process capability, documentation and repeatable delivery.
Frequently asked questions
What is the difference between bespoke precision engineering and standard machining?
Standard machining follows established routes for relatively familiar parts. Bespoke precision engineering adapts the design review, manufacturing route, inspection method and documentation around a specific requirement, especially when geometry, tolerance, material or application risk is unusual.
Is bespoke precision engineering always more expensive?
The unit price is often higher than a standard component, but total cost depends on the project. If a bespoke part reduces rework, assembly adjustment, downtime or field failure, it may be more economical over the full lifecycle.
Which tolerances should be tightened first?
Tolerances should be tightened only where they protect function, assembly or interchangeability. Tightening every dimension can increase cost and inspection burden without improving performance. Critical features should be identified through functional analysis and then linked to a clear inspection method.
Does ISO 9001 certification prove precision capability?
No. ISO 9001 relates to quality management system requirements. It can support consistent processes, but it does not by itself prove that a manufacturer can machine a specific material, hold a specific tolerance or inspect a specific feature. Capability should be assessed against the actual part, process and evidence required.
What information should be included in a request for quote?
A strong request should include drawings or models, material requirements, quantities, revision level, critical tolerances, surface finish needs, inspection documentation, delivery expectations and any special packaging, cleaning or traceability requirements. Clear information helps suppliers quote the real engineering work rather than adding risk allowances for unknowns.