Borescope inspection for aircraft engines and what maintenance teams should check
Why borescope inspection matters in aircraft engine maintenance
Aircraft engine borescope inspection procedures are used to examine internal areas that cannot be viewed directly without major disassembly. In service, the method supports faster fault isolation, better maintenance planning, and more defensible airworthiness decisions. It does not replace the engine maintenance manual, service bulletins, airworthiness directives, or required release-to-service records.
The strongest inspection programs treat the borescope as one part of a wider evidence chain: inspection access, image quality, defect recognition, measurement, trend history, oil or chip data, engine operating symptoms, and approved acceptance limits. Two inspections using the same camera can therefore produce very different value. Equipment matters, but procedure, training, documentation, and engineering disposition usually matter more. You can also explore more in tooling and inspection.
What a borescope inspection actually does
A borescope is a remote visual inspection tool. In aviation maintenance, it is commonly inserted through spark plug holes, igniter openings, dedicated access ports, fuel nozzle openings, or other approved access points so the inspector can view internal engine surfaces. Older tools relied on rigid or flexible optical paths. Modern videoscopes often add digital imaging, articulation, measurement functions, and still-image or video capture.
The goal is not simply to “look inside.” A useful engine borescope inspection answers defined maintenance questions. Is a cylinder showing valve distress, corrosion, oil pooling, scoring, or abnormal deposits? Has a compressor or turbine blade suffered foreign object damage, erosion, cracking, burning, coating loss, tip rub, or missing material? Are combustor liners, nozzles, seals, shrouds, or vanes still within the serviceable limits defined by approved data?
FAA Advisory Circular 43-204, Visual Inspection for Aircraft, has long described borescopes as tools for inspecting otherwise inaccessible aircraft areas. It also lists typical aircraft uses, including engine cylinder sleeves, pistons, valves, and aircraft turbines for cracks, corrosion, foreign object damage, and erosion. That broad scope is why borescope inspection appears in both general aviation piston maintenance and transport-category turbine engine programs.
Where borescope inspection fits in the maintenance system
The controlling reference is normally the engine manufacturer’s maintenance manual, instructions for continued airworthiness, an approved inspection program, or an applicable airworthiness directive. A borescope image alone does not make a part serviceable. The finding must be compared with the correct limits for that engine model, part number, serial configuration, operating environment, and maintenance program.
For U.S. annual and 100-hour inspections, 14 CFR Part 43 Appendix D requires inspection of the engine and nacelle group, including internal-engine checks such as cylinder compression and checks for metal particles or foreign matter on screens and sump drain plugs. Appendix D does not make borescope inspection mandatory for every engine at every annual inspection. Instead, maintenance teams commonly use it to add visibility when compression readings, oil analysis, operating symptoms, service history, or manufacturer instructions justify a closer look.
For turbine engines, the role can be more formal. FAA Advisory Circular 33.90-1A, issued on April 13, 2016, provides guidance for initial maintenance inspection under 14 CFR 33.90. In its on-wing inspection discussion, it includes full borescope inspection of accessible gas-path stages or areas of the fan, compressor, combustor, and turbine modules to the serviceable limits of the instructions for continued airworthiness. This does not mean every line-maintenance task is identical, but it shows how central remote visual inspection has become in turbine-engine airworthiness evaluation.
Airworthiness directives add another layer. The FAA states that ADs are legally enforceable rules issued under 14 CFR Part 39 to correct unsafe conditions in products such as engines. When an AD requires a borescope inspection, the compliance time, affected model, affected part, inspection method, and follow-on action must be read exactly. Operators should search both the engine model and the specific series or variant, because applicability can be narrower than the engine family name suggests.
What inspectors look for inside different engine areas
The defect list depends on engine type and inspection task. A piston engine cylinder inspection is not the same as a high-pressure turbine blade inspection, and a post-bird-strike inspection is not the same as a scheduled trend inspection. The table below summarizes typical areas and why they matter.
| Inspection area | Typical concerns | Why it matters |
|---|---|---|
| Piston engine cylinder | Exhaust valve burning, intake valve condition, cylinder wall scoring, corrosion, piston crown deposits, oil pooling | Helps interpret compression results and identify conditions that may not be obvious from pressure readings alone |
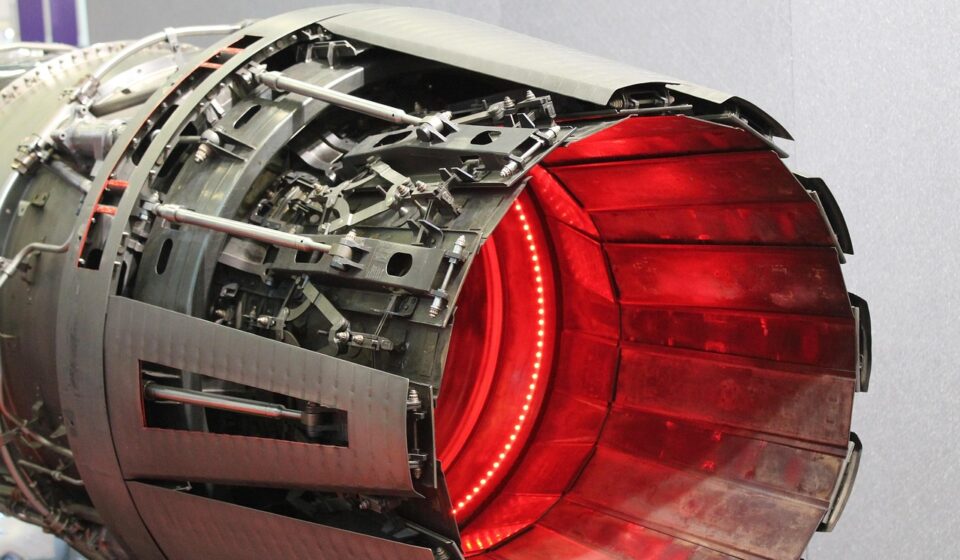
| Fan and compressor | Foreign object damage, leading-edge nicks, erosion, blade tip rub, deposits, corrosion | Damage can affect airflow, efficiency, vibration, and downstream engine health |
| Combustor section | Cracking, burn-through, hot spots, liner distress, fuel nozzle-related distress | Combustion-zone damage can progress quickly and may create thermal stress in downstream parts |
| Turbine blades and vanes | Cracks, missing material, coating loss, oxidation, blade distress, nozzle vane damage | Turbine components operate in severe thermal and mechanical conditions and often drive removal decisions |
| Seals, shrouds, and abradables | Rub, coating distress, honeycomb damage, excessive wear | Clearance control affects performance, temperature margin, and component life |
The important point is that a defect name is not enough. “Crack,” “burn,” or “missing material” must be tied to location, orientation, size, affected surface, repeatability of the observation, and the applicable service limit. Where measurement is required, the inspection procedure should specify whether a stereo measurement, shadow measurement, comparison gauge, or other approved method is acceptable.
Planning a reliable borescope inspection
A strong borescope inspection starts before the probe enters the engine. The work package should identify the reason for inspection, reference data, engine status, access points, required equipment, cooling requirements, safety precautions, and documentation standard. For turbine engines, access-port naming and viewing direction are critical. Missing one access path can leave a high-risk zone unexamined, even if the record says a borescope inspection was performed.
Temperature control is often overlooked. FAA AC 43-204 includes sample engine borescope guidance warning that hot internal areas can damage equipment and create safety hazards. Many engine procedures also require defined cool-down conditions before optical equipment is inserted. The practical rule is simple: schedule pressure should never override the engine manual, tooling instructions, or safe handling limits.
Image quality is another limiting factor. Poor lighting, dirty lenses, fogging, weak articulation, incorrect probe diameter, excessive glare, or unstable rotor positioning can turn a potentially useful inspection into a weak record. A useful image should show enough surrounding geometry to confirm location, not only a close-up of damage. For repeat inspections, matching the viewing angle and saving comparable images helps maintenance teams determine whether damage is stable, improving, or progressing.
Personnel capability is equally important. ISO 9712:2021 covers qualification and certification requirements for personnel performing industrial non-destructive testing methods, including visual testing within its scope. Aviation operators may use different regulatory and company qualification systems, but the underlying lesson is consistent: defect recognition, visual acuity, procedure discipline, and reporting competence are part of the inspection system, not optional extras.
How findings should lead to maintenance decisions
A borescope finding should normally lead to one of four outcomes. First, the inspected area is acceptable and the engine remains in service under the normal program. Second, the area is acceptable but requires closer monitoring or a shortened repeat interval. Third, the finding exceeds limits and requires repair, replacement, or removal before further operation. Fourth, the image is inconclusive and additional inspection, cleaning, repositioning, or another NDT method is needed. See also: cnc and robotics.
Good decisions avoid two common errors. The first is overconfidence: treating a low-cost camera image as if it overrides approved data. The second is underuse: performing a borescope inspection but failing to connect findings to operating symptoms, trend data, chip detector results, oil filter evidence, vibration reports, exhaust gas temperature changes, or prior images. Internal visual evidence is more valuable when it becomes part of a traceable history.
Documentation should include the engine identification, aircraft identification if applicable, date, time or cycle reference, reason for inspection, governing reference, access ports used, areas examined, equipment used when required by procedure, results, images or video location, measurement method, inspector identity, and any required maintenance record entry. FAA AC 43-9D, issued on September 22, 2025, addresses maintenance recordkeeping and reinforces that work performed on aircraft engines must be recorded in a way that supports regulatory compliance and return-to-service decisions.
Recent FAA examples show why the details matter
Public FAA documents show that borescope inspection is not only a generic shop practice. It can become a targeted risk-control action when field experience reveals a specific unsafe condition.
One example is FAA Special Airworthiness Information Bulletin NE-16-19, dated July 22, 2016, involving certain Honeywell TPE331-10 and TPE331-11 turboprop engines. The FAA reported 21 first-stage turbine blade failures between October 1997 and November 2013, including 15 in-flight shutdown events. The bulletin recommended borescope inspection at every fuel nozzle inspection interval, not to exceed 450 hours since the last inspection, and recommended viewing through four fuel nozzle boss openings to obtain full coverage of the first-stage nozzle. Because the SAIB was advisory rather than mandatory, it also illustrates the difference between safety information and an enforceable AD.
A more recent example is FAA AD 2026-14-06 for certain CFM LEAP-1A engines. Issued in July 2026, it superseded AD 2025-21-03 and required initial and repetitive borescope inspections of high-pressure turbine rotor stage 1 blades for affected configurations. The FAA linked the action to two in-flight shutdowns and blade cracks, and the rule addressed accelerated blade deterioration and airfoil distress associated with South Asia operation and dust buildup. For affected Group 1 engines, the repetitive interval was not to exceed 150 flight cycles; for affected Group 2 engines, it was not to exceed 300 flight cycles. The same document estimated a borescope inspection labor cost of four work-hours at $85 per hour, or $340 per product, while replacement of the blade set was estimated at a much higher on-condition cost.
The maintenance lesson is clear. The value of borescope inspection is not only in finding visible damage. It is also in creating a repeatable inspection path that regulators, manufacturers, operators, and maintenance organizations can connect to defined risk, defined thresholds, and defined corrective action.
Frequently asked questions
Is borescope inspection mandatory for every aircraft engine?
No. It depends on the aircraft, engine, inspection program, manufacturer instructions, service bulletins, operating symptoms, and any applicable airworthiness directive. Some tasks make borescope inspection required; in other cases it is a useful diagnostic or preventive-maintenance aid.
Can a borescope inspection replace a compression check?
For piston engines, it usually complements rather than replaces compression testing unless the governing maintenance data says otherwise. Compression readings, borescope images, oil evidence, engine history, and operating symptoms provide different evidence about internal condition.
What is the difference between a borescope and a videoscope?
A borescope is the broad category of remote visual inspection tool. A videoscope is a digital version that uses a camera and display, often with articulation, image capture, and measurement features. Many modern aviation maintenance teams use videoscopes while still referring to the task as borescope inspection.
Who should interpret aircraft engine borescope findings?
Findings should be interpreted by qualified personnel using the correct engine manual, inspection procedure, approved data, and operator authorization system. When limits are unclear or damage is unusual, engineering or manufacturer support may be necessary before return-to-service decisions are made.
What makes a borescope report useful?
A useful report identifies the engine, access point, inspected area, applicable reference, finding location, image evidence, measurements when required, disposition, and next action. Comparable images from earlier inspections add significant value because they show whether a condition is stable or progressing.
Bottom line for maintenance teams
Borescope inspection gives maintenance teams a practical way to see inside an aircraft engine without unnecessary teardown, but its value depends on disciplined execution. The best programs define the inspection question, use approved procedures, capture repeatable evidence, compare findings with service limits, and document the result in the maintenance record. For more coverage of inspection tools and manufacturing quality topics, visit the tooling and inspection section.