Nut and bolt manufacturing machine line for cold forming, threading and inspection
What a nut and bolt manufacturing machine line actually includes
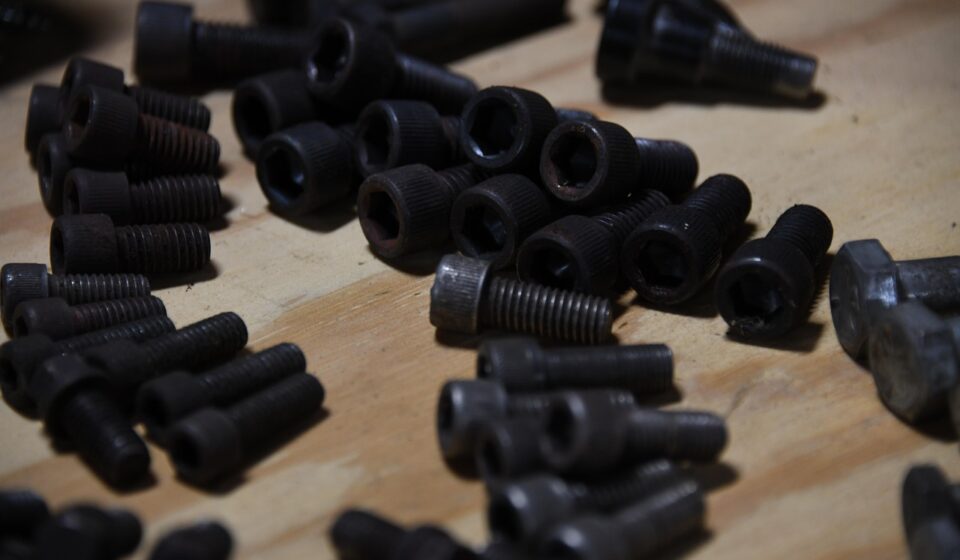
A nut and bolt manufacturing machine is usually not a single machine. In industrial fastener production, it is a connected line of forming, threading, heat treatment, finishing and inspection equipment, matched to a defined fastener range. For bolts, the core equipment typically includes wire preparation machines, cold headers or part formers, pointing units, thread rolling machines, heat treatment furnaces, coating systems and sorting equipment. For nuts, the line normally includes wire or bar preparation, nut formers, piercing or punching stations, tapping machines, heat treatment where required, surface finishing and inspection.
The right line depends less on whether the product is called a nut or a bolt, and more on diameter, material, head style, thread type, property class, production volume and inspection requirements. For manufacturers, the main question is not only machine speed. It is whether the complete process can repeatedly produce parts that meet dimensional, mechanical and surface requirements.
A fast header with weak tooling control, unstable tapping or poor inspection can produce scrap faster than a slower, better-controlled line. Tooling life, thread quality, heat treatment uniformity and inspection strategy should therefore be evaluated together, not as separate purchasing decisions.
The basic production flow for bolts
Most standard carbon steel and alloy steel bolts are made by cold forming when the size, material and geometry allow it. Cold forming is widely used because it creates near-net shapes with high material utilization and high output. Larger parts, very long parts, unusual geometries or parts requiring high deformation may need hot forging, warm forming, machining or a hybrid process.
Wire preparation and cold heading
Bolt production normally starts with wire rod or coil. The material may pass through spheroidizing annealing, pickling, phosphating and drawing before heading. These steps improve formability, remove scale, provide lubrication and bring the wire to the required diameter.
In cold heading, a cut blank is upset in dies to form the head and shank geometry. Multi-station headers can form more complex shapes progressively, while simpler one-die, two-blow machines are used for less complex parts.
The tooling set is critical at this stage. Dies, punches, cutters and transfer fingers must match the material strength, blank length, head shape and forming ratio. Poor tooling alignment can cause eccentric heads, laps, cracks, short fill or excessive tool wear. For production planning, the tooling and inspection plan should be considered before the line is purchased, not after the first trial run.
Pointing and thread rolling
After heading, many bolts are pointed or chamfered so they can enter the threading operation cleanly. Thread rolling is common for mass-produced bolts because it forms the thread by plastic deformation between flat or cylindrical dies. Compared with cutting, thread rolling does not remove material and can preserve a favorable grain flow around the thread. Public technical references on fastener production also note that cutting is possible, but it is generally slower for standard high-volume fasteners.
Thread rolling machines must be selected according to thread length, diameter, pitch, material strength and required production rate. Flat-die thread rollers are common for standard bolts and screws. Cylindrical-die machines may be suitable for long threads, special profiles or secondary operations. The process is sensitive to blank diameter, die wear, lubrication and feed control. Even a small change in blank diameter can shift pitch diameter and lead to go/no-go gauge failures.
Heat treatment and surface finishing
Many high-strength bolts require quenching and tempering to reach the intended property class. ISO 898-1:2013, which covers bolts, screws and studs made of carbon steel and alloy steel with specified property classes, states that mechanical and physical properties are tested at an ambient temperature range of 10 °C to 35 °C. This is one reason the production line cannot be evaluated only up to the thread rolling stage. Heat treatment can change hardness, tensile strength, ductility and surface condition.
Surface finishing may include black oxide, zinc plating, zinc flake coating, phosphate, oiling or other treatments depending on the application. Coating thickness can affect thread fit, so finishing must be considered together with thread tolerance. When electroplating is used on high-strength fasteners, manufacturers also need a controlled approach to hydrogen embrittlement risk, including appropriate baking and testing when specified by the product standard or customer requirement.
The basic production flow for nuts
Nut production shares some preparation steps with bolt production, but the forming and internal threading operations are different. A nut manufacturing line is often built around a nut former, tapping equipment and sorting systems. The forming sequence creates the outside shape and hole, while tapping creates the internal thread.
Cold forming, punching and trimming
Hex nuts are commonly cold formed from wire or bar stock when the material and size range are suitable. A nut former cuts blanks and forms the external geometry through multiple stations. The central hole is created by punching or piercing, and the part may be trimmed to establish flats, chamfers and height. Punch and die design must control hole position, wall thickness and outer geometry because errors at this stage cannot always be corrected during tapping.
For nuts, concentricity and hole quality are especially important. If the hole is off-center, tapping can produce uneven thread engagement. If the punched hole has burrs, laps or cracks, the internal thread may fail inspection or cause assembly problems. A nut line should therefore be evaluated not only by rated pieces per minute, but also by scrap rate, punch life, die maintenance and stability during long production runs.
Tapping and nut property classes
Tapping machines cut or form the internal thread depending on the machine design and material. High-volume nut tapping usually requires automatic feeding, reliable orientation, chip control and tool monitoring. Taps are consumables, and a worn tap can create oversized threads, poor flank finish or incomplete engagement before visible defects are obvious to the operator.
ISO 898-2:2022 covers mechanical and physical properties for nuts made of non-alloy steel or alloy steel with specified property classes. The standard applies to ISO metric threads within defined coarse and fine pitch ranges and includes regular nuts, high nuts and thin nuts. It also addresses nut property classes such as 04, 05, 5, 6, 8, 10 and 12. In practice, this means the nut manufacturing machine line must be able not only to make a hex shape and internal thread, but also to support the proof load, hardness and mating performance required for the specified class.
Key machines in a fastener production line
| Process stage | Typical equipment | Main control point | Common quality risk |
|---|---|---|---|
| Wire preparation | Annealing, pickling, coating and drawing equipment | Diameter, surface condition and formability | Cracking, poor lubrication or inconsistent blank size |
| Bolt forming | Cold header or multi-station part former | Blank length, die alignment and forming sequence | Head cracks, eccentricity, laps or underfill |
| Nut forming | Nut former, punch and trimming tooling | Hole position, wall thickness and flats | Off-center holes, burrs or distorted geometry |
| External threading | Flat-die or cylindrical thread rolling machine | Blank diameter, die condition and thread pitch | Pitch diameter failure, torn threads or die marks |
| Internal threading | Automatic nut tapping machine | Tap wear, feed, lubrication and chip control | Oversized threads, incomplete threads or broken taps |
| Heat treatment | Continuous furnace, quench system and tempering furnace | Temperature, time, atmosphere and quench control | Hardness variation, decarburization or distortion |
| Finishing | Plating, coating, washing and drying systems | Coating thickness and surface cleanliness | Thread fit issues, corrosion risk or embrittlement concerns |
| Inspection | Gauges, hardness testers, tensile equipment and optical sorting | Sampling plan and defect detection capability | Mixed parts, missed cracks or undocumented nonconformance |
Inspection requirements should shape the machine choice
Inspection is not an afterthought at the end of the line. It should influence machine selection from the beginning. A high-output line may need automatic optical sorting, eddy current crack detection, hardness testing, thread gauging and clear lot traceability. A lower-volume special fastener line may rely more on dimensional inspection, calibrated gauges and laboratory testing, but it still needs a defined acceptance plan.
ASTM F606/F606M-21 is a widely used test-method standard for determining mechanical properties of externally and internally threaded fasteners, washers, direct tension indicators and rivets. It describes procedures such as product hardness, proof load, axial tension, wedge tension and nut proof load testing. ISO 898-1 and ISO 898-2 define property requirements for many metric bolts and nuts. ASME B18.2.1 covers inch-series square, hex, heavy hex and related bolts and screws. Heavy hex structural bolts are covered separately under ASME B18.2.6. See also: cnc and robotics.
For readers comparing tooling, gauges and process control methods, the tooling and inspection section provides related manufacturing context. In fastener production, inspection usually combines several methods rather than relying on one universal test.
- Dimensional inspection: checks head height, across-flats dimension, shank diameter, length, chamfer, nut height and hole position.
- Thread inspection: uses go/no-go gauges, ring gauges, plug gauges and pitch diameter checks where required.
- Mechanical testing: includes hardness, proof load, tensile or wedge tensile testing depending on product type and standard.
- Surface inspection: looks for cracks, folds, laps, plating defects, scale, rust, dents and mixing of nonconforming parts.
- Coating verification: checks coating thickness, adhesion, appearance and thread fit after finishing.
- Lot traceability: links raw material, heat treatment, machine setup, inspection results and packaging to a defined production lot.
How to select the right nut and bolt manufacturing machine
The best equipment choice is usually the one that matches the product family with the least process risk. Before comparing quotations, define the parts that will actually be produced: diameter range, length range, head style, nut style, thread pitch, material grade, property class, coating and annual volume. A machine that is excellent for standard M8 bolts may be unsuitable for long studs, large-diameter hot-forged bolts or thin nuts with tight height control.
Product range and forming complexity
Station count matters. More forming stations allow more gradual deformation, which can reduce cracking risk and enable complex shapes. However, more stations also mean higher tooling cost, longer setup time and more maintenance points. For a narrow, high-volume product, a dedicated machine may be economical. For a job shop or mixed fastener supplier, flexibility and changeover efficiency may be more valuable than maximum rated speed.
Material and strength class
Low-carbon steel, medium-carbon steel, alloy steel and stainless steel behave differently during heading, rolling and tapping. Higher-strength or less ductile materials may require different wire preparation, stronger machine frames, better lubrication and more robust tooling. If the final fastener requires a higher property class, heat treatment and testing capacity must also be planned.
Tooling, maintenance and operator skill
Fastener machines are productive only when tooling is controlled. Dies, punches, thread rolling dies and taps must be available, measurable and replaceable. Buyers should ask how quickly tooling can be changed, how adjustments are made, whether setup data can be recorded, and how the machine detects jams or abnormal load. Operator skill remains important, especially for first-article approval, troubleshooting and tool wear judgment.
Automation and sorting
Automatic feeding, part transfer, in-line gauging and optical sorting can reduce labor and improve consistency, but automation should be justified by defect risk and volume. For safety-critical or high-volume fasteners, automatic sorting can remove parts with missing threads, wrong dimensions, visible cracks, damaged heads or mixed sizes. For smaller batches, a well-designed sampling and gauge plan may be more practical.
Common mistakes when planning a fastener line
One common mistake is buying a machine based only on catalog speed. Rated speed is often measured under favorable conditions. Real output depends on material quality, tooling condition, setup time, maintenance, inspection hold points and downstream capacity. A thread roller cannot solve instability created by poor blank control, and a sorting machine cannot make a weak heat treatment process acceptable.
Another mistake is treating nut and bolt production as the same investment. They share some material preparation and finishing operations, but the core forming and threading processes differ. Bolts need reliable heading and external thread rolling. Nuts need stable forming, hole control and tapping. Forcing both products through unsuitable equipment can create high scrap and inconsistent quality.
A third mistake is ignoring standards until the customer asks for certificates. If a product is sold as a specific property class or to a specific dimensional standard, the required inspection and documentation should be designed into the line. The machine purchase should include capacity for gauges, testing, calibration, records and segregation of nonconforming parts.
A practical checklist before purchasing
- Define the exact fastener families by size, material, thread and standard.
- Confirm whether cold forming, hot forging, machining or a hybrid route is appropriate.
- Match station count and machine force to the most difficult part, not only the easiest one.
- Review tooling availability, expected tool life and changeover procedure.
- Check thread rolling or tapping capacity against required thread length and pitch.
- Plan heat treatment and coating around the mechanical and dimensional requirements.
- Specify inspection equipment, sampling frequency and lot traceability before production starts.
- Evaluate realistic output after setup, maintenance and inspection, not just rated machine speed.
Frequently asked questions
Is a nut and bolt manufacturing machine one machine?
Usually no. In industrial production, it is normally a production line made up of wire preparation equipment, forming machines, threading machines, heat treatment, coating and inspection systems. Small workshops may use fewer machines or more manual handling, but reliable production still requires the same basic process controls.
Can the same machine make both nuts and bolts?
Some upstream and downstream equipment may be shared, such as wire preparation, heat treatment, coating and packaging. However, the core forming and threading machines are usually different. Bolts require heading and external thread rolling, while nuts require nut forming and internal tapping.
Is thread rolling better than thread cutting for bolts?
For many standard high-volume bolts, thread rolling is preferred because it is fast, uses material efficiently and forms threads by deformation rather than cutting. Thread cutting remains useful for some special sizes, low volumes, hard materials or geometries that are not suitable for rolling.
What inspection equipment is needed for fastener production?
The minimum inspection setup depends on the fastener standard and customer requirements. Common tools include calipers, micrometers, go/no-go thread gauges, ring or plug gauges, hardness testers, tensile or proof load testing equipment, coating thickness gauges and optical sorting systems for high-volume production.
Which standards are commonly considered?
For metric carbon steel and alloy steel fasteners, ISO 898-1 covers many bolts, screws and studs, while ISO 898-2 covers many nuts with specified property classes. ASTM F606/F606M provides test methods for mechanical properties. For inch-series dimensions, ASME B18 standards such as B18.2.1 and B18.2.6 are often relevant depending on product type.