How to choose a TIG welding machine for precision metal fabrication
What a TIG welding machine needs to do
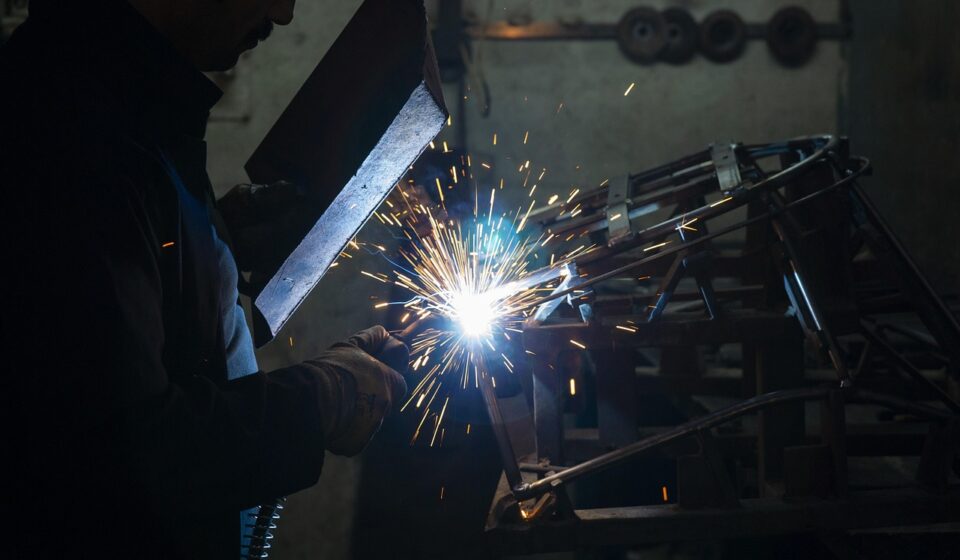
A TIG welding machine is built for gas tungsten arc welding, a process that uses a non-consumable tungsten electrode, an inert shielding gas and, where required, separate filler metal. Its main advantage is control. Compared with faster, higher-deposition welding processes, TIG is often chosen for clean weld beads, precise heat input, thin-material control and high-quality work on stainless steel, aluminum, titanium, nickel alloys or critical visible joints.
The right machine is not simply the model with the highest amperage rating. A shop should look at current type, low-amp stability, AC capability, arc starting method, pulse control, duty cycle, torch cooling, gas delivery and operator interface. These details affect weld quality, rework, training time and the range of materials the shop can handle. For more equipment context across fabrication and workshop systems, visit the machine tools section.
Start with the metals and weld requirements
The first buying decision is the material mix. A DC-only TIG machine can be an efficient choice for carbon steel, stainless steel and many nickel or copper alloys. Aluminum and magnesium usually require an AC-capable machine because alternating current helps manage the oxide layer while maintaining weld penetration. If a shop may add aluminum work later, a DC-only unit can quickly become a limitation.
Thickness range matters just as much. Thin sheet and tube work require stable arc starts at very low current, fine amperage adjustment and smooth remote control. Heavier sections need enough output and duty cycle to keep welding without repeated thermal shutdowns. A machine that performs well for occasional bench repairs may not be suitable for long production welds, pressure components or fixture-based repetitive work.
| Common workpiece | Typical TIG machine need | Key buying point |
|---|---|---|
| Carbon steel | DC TIG capability | Stable arc, suitable amperage range and good remote control |
| Stainless steel tube or sheet | DC TIG with excellent low-current control | Pulse, gas post-flow and consistent starts help reduce overheating and discoloration |
| Aluminum | AC/DC TIG capability | AC balance, frequency control and enough output for the section thickness |
| Titanium and reactive alloys | Precise DC TIG with strong gas coverage | Gas shielding discipline, clean setup and process control are critical |
| Repair and maintenance work | Portable inverter or multi-process-capable setup | Input power flexibility and rugged connectors may matter more than advanced menus |
Power source features that affect weld quality
Modern TIG machines are commonly inverter-based because inverters offer compact size, efficient power conversion and detailed control settings. Older transformer machines can still be durable and useful, but they are usually heavier and may offer fewer control functions. For a new purchase, the practical question is not inverter versus transformer on its own. It is whether the machine delivers the arc behavior, service support and duty cycle the application needs.
Amperage range should be checked from both ends. High output helps on thicker material, but a clean low-amp start is essential for thin stainless steel, small-diameter tube, edge welds and cosmetic work. Buyers should confirm that the machine can start and maintain a stable arc at the low current required for the smallest parts they expect to weld.
Arc starting method is another quality factor. High-frequency start allows the welder to initiate the arc without touching the tungsten to the workpiece, which helps avoid tungsten contamination. Lift-arc starting is useful where high-frequency interference is a concern, but it still depends on proper technique. Scratch start is simple, but it is less suitable for precision TIG work because it can contaminate the electrode and work surface.
Pulse welding is useful when the goal is heat control rather than speed. By alternating between peak and background current, pulse settings can help manage distortion and burn-through on thin material. Pulse is not a substitute for joint preparation or operator skill, but it gives a trained welder more control over heat input, bead profile and travel rhythm.
AC/DC selection, duty cycle and input power
An AC/DC TIG welding machine is the more flexible choice when a shop handles both ferrous and non-ferrous work. AC balance and AC frequency controls are especially relevant for aluminum. Balance affects the relationship between cleaning action and penetration, while frequency influences arc focus and puddle behavior. Operators who weld aluminum regularly benefit from controls that are clear, repeatable and easy to access.
Duty cycle describes how long a machine can weld at a specified output within a defined time period before it must cool. It is often overlooked because buyers focus on peak amperage. In production, a machine with a stronger duty cycle at the working amperage may be more useful than a cheaper model with a high maximum rating it cannot sustain. For bench fabrication, repairs or intermittent tack welding, the requirement may be lower. For long seams, heavy fixtures or repetitive shop work, duty cycle should be treated as a core specification.
Input power also deserves attention. Some machines support multiple input voltages, which is useful for field service or mixed shop environments. Output capacity may change depending on the input supply, however. Before purchase, confirm whether the shop’s electrical service, breaker size, plug configuration and extension-cord practices can support the output level expected in daily work.
Torch, tungsten electrode and shielding gas choices
The power source is only one part of the TIG system. Torch size, cable flexibility, cooling method, tungsten selection and shielding gas delivery all influence results. An air-cooled torch is simpler and adequate for many light and medium tasks. A water-cooled torch is better suited to higher amperage and longer welds because it reduces heat at the torch head and improves operator comfort.
Tungsten electrode selection should follow recognized classifications rather than color alone. ISO 6848:2015 covers classification of non-consumable tungsten electrodes for inert gas shielded arc welding and related processes, and that standard was reviewed and confirmed as current in 2026. The American Welding Society also lists AWS A5.12M/A5.12:2024 for tungsten and oxide-dispersed tungsten electrodes. These standards matter because electrode chemistry affects arc starting, stability and suitability for AC or DC welding.
Shops should be cautious with thoriated tungsten. It has been widely used in TIG welding, but it contains thorium oxide and requires appropriate handling, grinding dust control and disposal practices. Many shops now choose lanthanated, ceriated or other alternatives depending on machine type, polarity and application. The safest approach is to follow the electrode supplier’s safety data sheet and the shop’s written safety procedure.
Shielding gas is usually argon for many TIG applications. Helium or argon-helium mixes may be used where more heat input or different arc characteristics are needed, but gas choice should be matched to the metal, thickness, weld position and procedure requirements. Gas flow that is too low can allow atmospheric contamination. Flow that is too high can create turbulence and pull air into the shielding zone. A good regulator or flowmeter, leak-free hoses and correct cup size are part of machine performance in practice.
Controls that improve repeatability in a real shop
For occasional repair work, simple controls may be enough. In production, repeatability becomes more important. Digital parameter storage, clear meters, pre-flow and post-flow adjustment, slope control and remote amperage control can reduce setup variation between operators. These features are not only convenient; they help protect weld consistency when the same part is welded repeatedly across shifts. See also: cnc and robotics.
Remote control can be handled with a foot pedal, fingertip control or automation interface. A foot pedal is common for bench work because the operator can adjust amperage while watching the puddle. Fingertip control may be better for out-of-position work where foot control is impractical. Automated TIG cells may require interface ports, repeatable current programs, wire-feed integration and compatibility with positioners or motion systems.
Maintenance should also be considered before purchase. TIG machines need clean connectors, sound torch cables, proper cooling-system care when water-cooled, and periodic inspection of gas hoses and electrical leads. A machine with difficult-to-source consumables or weak local support can cost more over its life than a higher-priced unit with readily available torches, collets, cups, cables and service parts.
Safety and compliance checks before buying
TIG is often described as a clean process, but that does not mean it is hazard-free. Welding can produce fumes, gases, ultraviolet radiation, hot surfaces and electrical hazards. OSHA’s general industry welding rules are located in 29 CFR 1910 Subpart Q, and OSHA also addresses ventilation and protection for welding, cutting and heating in construction settings under 29 CFR 1926.353. These rules are not a buying checklist by themselves, but they show why ventilation, PPE, training and work area controls must be planned together with the machine purchase.
Ventilation needs depend on material, coatings, filler metals, current settings, work location and exposure time. Stainless steel, coated metals and confined spaces require particular attention. Local exhaust ventilation may be needed even when visible fume levels seem low. Eye and skin protection must address arc radiation, and shielding screens may be needed to protect nearby workers from arc flash.
Electrical safety should not be treated casually. Leads, connectors, insulation, grounding and dry work conditions all matter. Gas cylinders must be secured, capped when required and handled according to workplace safety rules. If a shop welds in tanks, vessels or restricted spaces, confined-space procedures and atmospheric testing may be required before the work begins.
A practical TIG welding machine buying checklist
A useful specification review connects the machine to actual work instead of comparing brochure features in isolation. Before purchasing, define the material range, thickness range, joint types, expected weld length, production volume and operator skill level. Then compare machines against those requirements.
- Choose DC-only only if aluminum and magnesium are not part of the expected work.
- Choose AC/DC if the shop welds or may soon weld aluminum.
- Check low-amp stability for thin sheet, tubing and cosmetic welds.
- Compare duty cycle at the amperage the shop will actually use, not only maximum output.
- Confirm input voltage, breaker requirements and output limits at each input voltage.
- Review arc start options, especially high-frequency start and lift-arc start.
- Look for pulse control when heat input and distortion control are important.
- Match torch cooling to weld length and amperage.
- Verify availability of torches, cups, collets, tungsten electrodes and service parts.
- Plan shielding gas, ventilation, PPE and electrical safety before the first weld.
The common mistake is buying around a single headline number. Peak amperage, advanced pulse menus or a low purchase price may look attractive, but the best fit is the machine that gives stable starts, repeatable control and enough sustained output for the shop’s real work. In many fabrication environments, usability and support are as important as rated output.
Frequently asked questions
Is a TIG welding machine difficult to use?
TIG welding usually requires more coordination than MIG welding because the operator controls the torch, arc length, travel speed and often a separate filler rod. Stable arc starts, smooth amperage control and clear settings make learning easier. Clean base metal preparation and correct technique still remain essential.
Do I need an AC/DC TIG machine?
You need AC/DC capability if aluminum or magnesium welding is part of the work. If the shop only welds carbon steel, stainless steel or similar DC applications, a DC-only unit may be sufficient. For future flexibility, many fabrication shops choose AC/DC even if aluminum is not the first application.
What shielding gas is most common for TIG welding?
Argon is the common shielding gas for many TIG applications. Other gases or mixtures may be used for special materials or thicknesses, but they should be selected according to the welding procedure, base metal and desired arc behavior.
How much amperage should a TIG machine have?
There is no universal answer because amperage depends on material, thickness, joint design and travel speed. Instead of buying by maximum output alone, compare the required working amperage, duty cycle at that amperage and low-current stability for thin parts.
Can TIG welding be automated?
Yes. TIG can be used in manual, mechanized and automated systems. Automation may require a compatible power source, torch mounting, arc control, travel motion, filler-wire feeding and repeatable fixturing. It is most useful when weld quality and repeatability justify the added setup cost.