Welding machine selection guide for fabrication shops
What a welding machine must do in a modern shop
A welding machine should be selected for the work it has to repeat safely and consistently, not for a headline amperage rating alone. In a fabrication shop, the right choice depends on the welding process, base material, joint thickness, production volume, available input power, duty cycle and operator skill level. A small repair area may be best served by a portable multiprocess inverter. A production cell may need a dedicated MIG system with stable wire feeding, planned fume extraction and controls that can support procedure consistency or data capture.
The practical question is whether the machine can produce acceptable weld quality at the required pace while staying within the shop’s safety, power and maintenance limits. Welding still depends heavily on operator technique, but the equipment sets the available arc characteristics, heat input range, repeatability, accessory compatibility and uptime. For readers comparing welding with other shop equipment, our machine tools section provides broader manufacturing context.
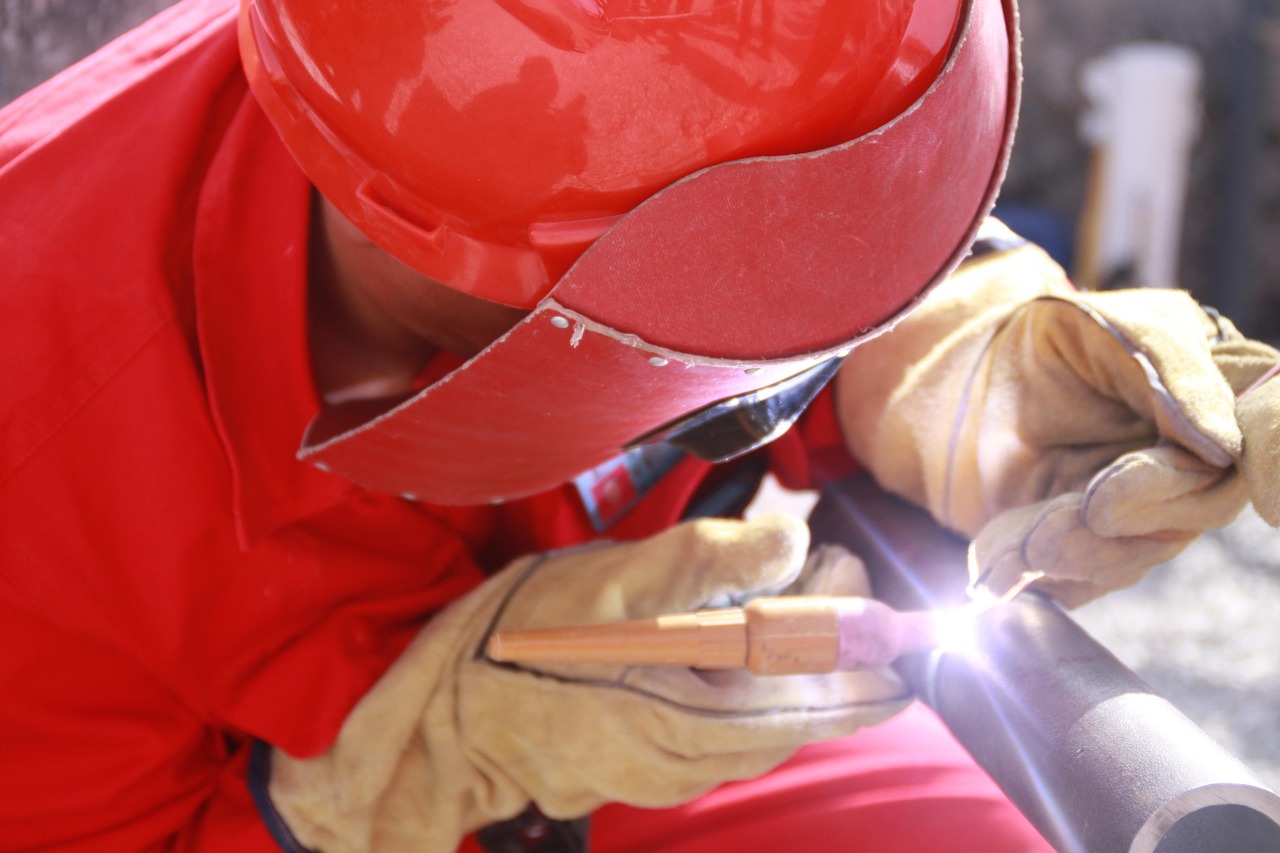
Match the welding process to the work
The term welding machine covers several equipment families. The starting point should be process fit, not brand preference or purchase price. American Welding Society terminology commonly distinguishes gas metal arc welding, gas tungsten arc welding, shielded metal arc welding and flux-cored arc welding. In shop language, these are usually called MIG, TIG, stick and flux-cored welding.
MIG or GMAW for repeatable fabrication
MIG welding, formally gas metal arc welding, uses a continuously fed wire electrode and shielding gas. It is widely used in fabrication because it can provide higher travel speed than stick welding and is relatively easy to standardize for repeatable joints. A MIG welding machine is often the practical choice for mild steel frames, brackets, cabinets, guards, fixtures and general production parts.
For MIG selection, the power source is only part of the system. Wire feeder performance, drive rolls, gun rating, liner condition, contact tips, gas delivery and workholding all affect weld consistency. If the work involves frequent changes in material thickness, machines with clear parameter control and saved programs can reduce setup variation.
TIG or GTAW for control and appearance
TIG welding, formally gas tungsten arc welding, uses a non-consumable tungsten electrode and usually a separate filler rod. It is slower than MIG in many production settings, but it gives the operator strong control over heat input and weld appearance. Shops often use TIG for stainless steel, aluminum, thin sections, precise assemblies, visible welds and repair work where distortion control matters.
When choosing a TIG-capable welding machine, check AC/DC output, high-frequency start or lift-arc start, pulse control, foot pedal compatibility and low-amperage stability. Aluminum TIG generally requires AC capability, while many steel and stainless applications use DC. A machine sold as multiprocess may support DC TIG but not AC TIG, so the process label by itself is not enough.
Stick and flux-cored for field work and heavy repair
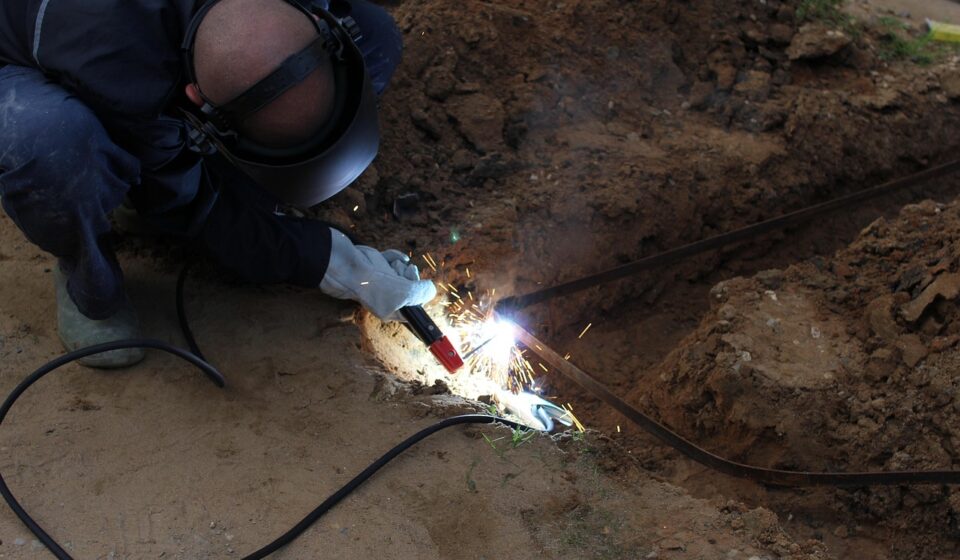
Stick welding, or shielded metal arc welding, remains useful because it is rugged, portable and tolerant of outdoor conditions when the correct electrode is used. It fits structural repair, maintenance, agricultural equipment, construction work and jobs where shielding gas cylinders are impractical.
Flux-cored arc welding uses a tubular wire with flux inside the electrode. Self-shielded flux-cored welding can be useful outdoors because it does not rely on external shielding gas in the same way as solid-wire MIG. Gas-shielded flux-cored welding can also offer high deposition rates for heavier fabrication. Before buying, confirm that the machine supports the required wire type, polarity, output range and feeder performance for the intended application.
Power source specifications that actually matter
Spec sheets can be misleading when several machines list similar maximum amperage. For production use, the more important issue is how the machine performs at the amperage and voltage needed for the actual weld, over the real amount of arc-on time.
| Specification | Why it matters | What to check before buying |
|---|---|---|
| Output range | Determines whether the machine can handle both thin and thick work without poor control. | Compare the required amperage range with your most common material thicknesses and processes. |
| Duty cycle | Shows how long the machine can weld at a stated output before cooling is needed. | Read the duty cycle at the amperage you will actually use, not only at the lowest rating. |
| Input power | Affects installation cost and portability. | Confirm available voltage, phase, breaker capacity and extension-cord limitations. |
| AC/DC capability | Important for TIG and certain electrode applications. | Do not assume every multiprocess unit supports AC TIG for aluminum. |
| Wire feed system | Controls consistency in MIG and flux-cored welding. | Check drive-roll quality, spool size, gun compatibility and feeder adjustability. |
| Thermal protection | Protects the power source when duty cycle is exceeded. | Review how the machine signals overheating and how quickly it recovers. |
Duty cycle deserves close attention. A machine rated for high amperage at a low duty cycle may be acceptable for intermittent repair, but it can become a bottleneck in production. If a shop welds long beads, heavy joints or repeated parts, a higher-duty-cycle industrial machine may be more economical than a lower-cost unit that frequently stops for cooling.
Power input is another common constraint. Portable inverters have made welding equipment lighter and more flexible, but no machine can compensate for inadequate supply power. Before purchase, confirm the shop’s available voltage and phase, the distance from the power source to the work area, and whether other equipment will run on the same circuit.
Safety, ventilation and standards belong in the purchase decision
A welding machine is not a complete welding system unless safety and environmental controls are included in the planning. In the United States, OSHA’s general industry welding, cutting and brazing rules address fire prevention, personal protective equipment and ventilation, including stricter precautions for confined spaces. NIOSH also emphasizes that welding fume composition and health effects depend on the metals, coatings, process, exposure time and ventilation conditions.
For purchasing, this means a shop should evaluate more than arc performance. The machine may need suitable fume extraction, screens, grounding, cable management, cylinder storage, PPE and operator training. Stainless steel, galvanized material, cadmium-bearing coatings or painted surfaces can raise additional exposure concerns. If the job involves tanks, vessels or restricted spaces, confined-space procedures should be addressed before equipment is deployed.
Standards also help define the equipment category. IEC 60974-1 covers safety requirements for arc welding power sources intended for industrial and professional use, while IEC 60974-10 addresses electromagnetic compatibility for arc welding equipment and allied processes. Buyers do not need to memorize the standards, but they should verify that professional equipment is certified or tested for the markets where it will be used.
Automation and digital controls are changing the value calculation
Fabrication shops are increasingly looking at automation not only to reduce labor pressure, but also to stabilize quality. AWS industry publications in 2025 and 2026 described continued adoption of robotic welding, cobots, digital monitoring and data-supported weld documentation. At the same time, AWS has also noted that automation does not remove the need for skilled welding knowledge; it changes where that knowledge is applied. See also: cnc and robotics.
That distinction matters. A robotic cell can repeat a qualified weld with excellent consistency when parts are accurately fixtured and the program is correct. It is less forgiving when gaps, fit-up, material condition or part variation change unexpectedly. For high-mix, low-volume work, the first investment may be better fixturing, cleaner joint preparation, improved parameter control or a semi-automatic welding machine rather than full robotics.
Digital features can still be valuable without full automation. Modern welding machines may offer preset programs, pulse modes, synergic controls, USB data export, network connectivity or weld parameter logging. These features can support training, procedure control and troubleshooting. They should not be treated as substitutes for qualified procedures, inspection and operator competence.
A practical welding machine selection checklist
Before comparing quotations, define the job profile. A clear work profile helps prevent overbuying and separates useful capabilities from marketing language.
- Primary material: mild steel, stainless steel, aluminum, cast iron or mixed repair work.
- Thickness range: minimum and maximum thickness, plus the thickness used most often.
- Welding position: flat bench work, vertical, overhead, pipe, field repair or confined access.
- Process requirement: MIG, TIG, stick, flux-cored or multiprocess.
- Production pattern: occasional repair, batch fabrication, continuous production or automated cell.
- Power availability: 120 V, 240 V, three-phase supply, generator use or shop distribution limits.
- Consumables: electrodes, wire diameter, shielding gas, contact tips, liners and torch parts.
- Safety controls: fume extraction, screens, PPE, fire watch needs and confined-space procedures.
- Serviceability: local repair support, parts availability, torch compatibility and warranty terms.
- Future needs: aluminum work, pulse MIG, data logging, automation interface or heavier duty cycle.
For a small maintenance shop, a portable multiprocess inverter may be the most flexible option, especially if the work changes daily. For a fabrication line making similar steel assemblies, a dedicated MIG or pulse-MIG system with a robust feeder may deliver better productivity. For precision stainless or aluminum work, a TIG machine with stable low-end control and the correct AC/DC capability may be more valuable than a higher maximum output.
A common mistake is buying for the rare heaviest job while ignoring the daily weld. If 80 percent of the work is light-gauge steel, low-amperage arc control, wire feeding and setup speed may matter more than maximum amperage. If the shop regularly welds thick sections, then duty cycle, heat management and deposition rate become decisive.
Frequently asked questions
What type of welding machine is best for a fabrication shop?
For many general fabrication shops, a MIG welding machine is the first choice because it is productive, repeatable and well suited to mild steel assemblies. The best choice changes if the shop focuses on precision stainless, aluminum, field repair or heavy structural work. In those cases, TIG, stick, flux-cored or a multiprocess system may be more appropriate.
Is a multiprocess welding machine suitable for production?
It can be suitable for maintenance, prototyping and mixed low-volume work. For continuous production, a dedicated machine may offer better duty cycle, wire feeding, cooling and process optimization. The decision should be based on the actual weld schedule rather than the number of processes listed on the front panel.
How important is duty cycle when buying a welder?
Duty cycle is very important when welds are long, parts are thick or production is repetitive. It indicates how much arc-on time the machine can handle at a stated output before cooling is required. A low-duty-cycle machine may still work well for short repair welds, but it can slow a production cell.
Do digital welding controls replace operator skill?
No. Digital controls can help with repeatability, parameter setup and documentation, but they do not replace fit-up, joint preparation, torch angle, travel speed or weld inspection. They are most useful when combined with trained operators and clear welding procedures.
Should safety equipment be included in the welder budget?
Yes. Fume extraction, PPE, screens, cable management, grounding and fire prevention measures are part of the real cost of welding. A machine that fits the budget but forces unsafe ventilation or poor work practices is not a good equipment choice.
Final thoughts
The right welding machine is the one that fits the shop’s process, material, duty cycle, safety requirements and future production direction. Maximum amperage and low purchase price are easy to compare, but they rarely tell the full story. A better decision comes from mapping the daily work, checking power and ventilation constraints, reviewing standards and safety obligations, and deciding whether flexibility, productivity or precision is the main priority.
For fabrication shops, the most reliable approach is to choose equipment around the welds that must be made every week, then allow enough capacity for reasonable growth. That balance keeps the machine useful, the operators productive and the welding operation easier to manage over time.