Inspection mirror with magnet for tooling and inspection work
Why a magnetic inspection mirror matters in manufacturing
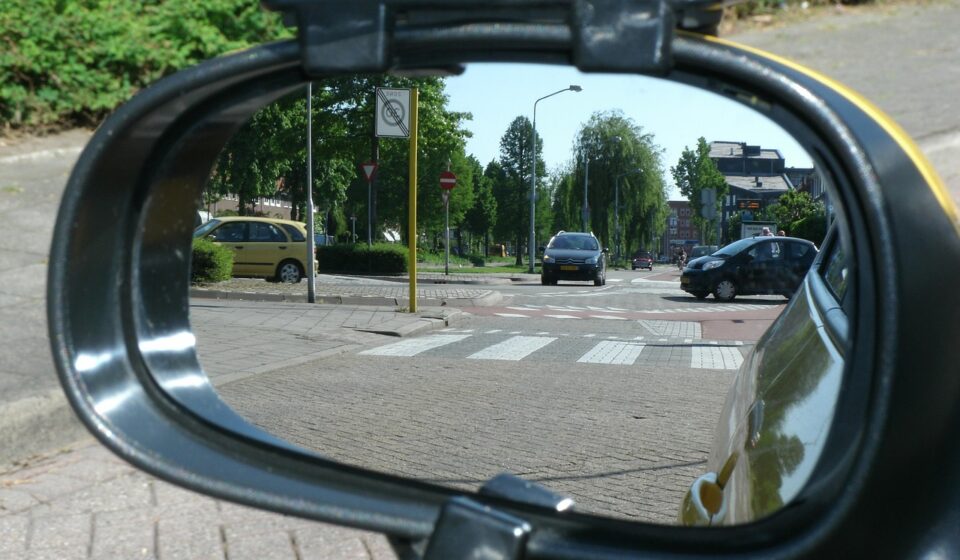
An inspection mirror with magnet is a simple tooling and inspection aid for viewing areas that are difficult to see directly. Typical examples include the back side of fixtures, hidden fasteners, internal shoulders, machine-tool corners, coolant lines, weld backs, casting pockets and under-machine spaces. The mirror does not measure a dimension, and it should not replace a borescope, CMM, gage or documented visual inspection method when those are required. Its value is speed, access and safety. A magnet lets the user park the tool on a machine frame, cabinet, bench, fixture or steel structure while freeing one hand for a flashlight, checklist or camera.
In mechanical manufacturing, the best use is not to “look everywhere.” It is targeted visual confirmation before, during or after a process step. A good mirror helps an operator answer practical questions: Is a cap screw seated? Is a burr visible on the far edge? Is the cutting insert chipped? Is a coolant leak starting behind the guard? Is a clamp contacting the intended surface? For more tooling references, see the tooling and inspection section.
What an inspection mirror with magnet can and cannot do
A magnetic inspection mirror is a visual access tool. It extends the inspector’s line of sight, but it does not improve the inspection method unless that method is already clear. That distinction matters in quality systems. ISO 9001:2015 clause 7.1.5 is commonly applied to monitoring and measuring resources, while dimensional conformance decisions may require traceable measuring equipment, defined acceptance criteria and a documented decision rule. A mirror can support inspection, but it is not normally a calibrated measuring instrument.
Useful applications include quick checks for assembly completeness, foreign-object debris, surface damage, missing labels, fastener presence, hose routing, weld accessibility, tool wear and cleanliness in hard-to-view locations. Maintenance teams also use these mirrors to inspect belts, pulleys, chain paths, cabinet backs, hydraulic fittings and pneumatic connections before disassembly.
The limits should be clear in work instructions. A mirror image can reverse orientation, distort scale and hide defects when the lighting angle is poor. Convex mirrors increase field of view but reduce detail. Small flat mirrors show more detail but require more precise positioning. Reflections on oily or highly polished surfaces can create false impressions. If a defect must be sized, recorded for acceptance, or compared with a specification, the mirror should be paired with an approved measuring or imaging method.
Key selection factors for shop-floor use
Choosing an inspection mirror with magnet is mainly a matter of matching access, lighting, durability and magnetic holding needs to the task. Overbuying can make the tool bulky. Underbuying can make it ineffective in deep fixtures or guarded spaces.
Mirror size and shape
Round mirrors are common because they are compact and easy to angle around obstructions. Rectangular mirrors provide a wider horizontal view and can be useful along seams, flanges and machine ways. Small mirrors fit into bores, pockets and gaps between fixture elements, while larger mirrors make general maintenance checks faster. For fine burr detection or edge condition checks, a smaller flat mirror with strong lighting is usually more useful than a large convex mirror.
Flat, convex and replaceable mirrors
A flat mirror gives a more natural view and is better for confirming detail. A convex mirror expands the viewing area and helps scan larger hidden zones, but it makes objects appear smaller. Replaceable mirror heads are practical in abrasive shops where chips, grinding dust or accidental drops can scratch the reflective surface. If the mirror will be used near coolant, oils or cleaning fluids, the head and adhesive should tolerate routine wiping.
Handle reach and articulation
Telescoping handles are useful around machine tools, weldments, large molds, dies and equipment cabinets. The extension should lock firmly enough that the head does not collapse when angled upward or sideways. Double-ball joints, swivel heads and flexible necks can help reach around clamps and ribs, but they need to hold position after repeated use. A tool that drifts under its own weight slows inspection and can encourage unsafe hand positioning.
Magnet strength and placement
The magnet may be built into the handle end, the base or a separate clip. A handle-end magnet is convenient for retrieving small ferrous hardware and parking the mirror on a machine surface. A magnetic base is better when the mirror must remain fixed during observation. In CNC and fabrication environments, magnet strength should be balanced against cleanliness: a very strong exposed magnet can collect chips and grinding debris, which may scratch surfaces or become a contamination source.
Lighting compatibility
Some inspection mirrors include an LED, while others rely on a separate flashlight or machine light. Built-in LEDs are useful inside cabinets, enclosures and shadowed fixtures, but batteries add maintenance. Separate lighting gives more control over angle and intensity. For detecting cracks, burrs and surface marks, side lighting often reveals more than straight-on illumination because it creates shadows at raised or broken edges.
Comparison of common magnetic inspection mirror types
| Type | Best fit | Strength | Limitation |
|---|---|---|---|
| Telescoping mirror with magnetic handle | General machine-shop checks, fastener presence, fixture inspection | Portable and inexpensive; easy to store in a toolbox | May shake at full extension and needs separate lighting |
| LED inspection mirror with magnet | Cabinets, guarded areas, shadowed machine corners | Combines viewing and illumination in one hand tool | Battery condition and coolant exposure must be managed |
| Magnetic-base inspection mirror | Maintenance observation, setup checks, repeated viewing angle | Can hold a fixed position and free both hands | Requires a clean ferrous mounting surface |
| Small flat mirror with magnetic pickup end | Burr checks, insert checks, tight pockets and small assemblies | Good detail in confined spaces | Narrow field of view and slower scanning |
| Convex mirror with magnet | Fast scanning behind panels, housings and guards | Wide field of view | Less suitable for judging fine defects |
This comparison is a practical starting point, not a ranking. The right mirror depends on access geometry, defect size, lighting, surface condition and whether the observation is informal troubleshooting or part of a controlled inspection plan.
How to use it safely around machines and fixtures
Safety is one reason many shops keep inspection mirrors near machines and fixtures. OSHA guidance for hand and power tools emphasizes hazard assessment, tool condition and keeping workers out of hazardous areas. In practice, a mirror should help the user avoid putting fingers, wrists or the face into pinch points, sharp chip zones, hot surfaces or locations near rotating equipment. It should not become a reason to inspect moving machinery at close range unless the procedure specifically permits it and guards, lockout requirements and safe distances are addressed.
- Stop the machine or follow the approved safe-state procedure before viewing areas near rotating tools, belts, spindles, gears or powered slides.
- Use the mirror to extend vision, not to push chips, move parts or contact cutting tools.
- Keep the magnet away from sensitive electronics, magnetic scales, encoders, credit-card style access badges and media that can be affected by magnetic fields.
- Clean chips from the magnet before placing it on precision surfaces, ground ways, fixture datums or finished parts.
- Do not rely on a mirror to verify clearance while a person is inside a guarded area unless the lockout and access procedure allows that work.
The most common misuse is treating the mirror like a hook or pry tool. Once the neck is bent, the joint is loose or the reflective surface is scratched, the image can become unreliable. A low-cost tool still needs basic control if it influences inspection decisions.
Building it into a controlled inspection workflow
For casual maintenance, a magnetic mirror may live in a toolbox. For production inspection, it should be linked to a defined purpose. The work instruction should identify what is being viewed, from which direction, under what lighting and what condition is acceptable. This prevents two inspectors from reaching different conclusions simply because one viewed the part from another angle. See also: cnc and robotics.
A practical work instruction might say: “Use a flat inspection mirror and white light to check the back edge of the pocket after deburring. No continuous raised burr visible along the edge.” That is more useful than “inspect pocket.” If a visual result affects part acceptance, the acceptance criterion should be written so that it can be repeated and audited.
Where measurement uncertainty or conformance decisions are involved, ASME B89.7.3.1 and NIST guidance on measurement uncertainty are useful reminders that inspection decisions should account for the capability and limits of the method. A mirror can reveal that a burr exists, but it cannot assign a reliable height unless it is combined with an appropriate measuring method. For high-risk characteristics, the mirror may be a screening tool that triggers a documented follow-up inspection.
Records do not have to be complicated. Some shops use a checkbox in a setup sheet; others attach a photo taken through or near the mirror when access is difficult. The key is traceability: the record should show that the hidden feature was checked, not merely that a general operation was completed.
Care, storage and replacement checks
Inspection mirrors are often damaged because they are treated as disposable. A scratched or cloudy mirror can hide small surface defects, especially under coolant mist or low light. A loose pivot can change the viewing angle during inspection. A magnet packed with chips can scratch equipment or contaminate clean assemblies. These are small issues, but they reduce confidence in visual checks.
- Wipe the mirror face with a soft cloth after use, especially after exposure to coolant, oil, grinding dust or weld spatter.
- Remove metal chips from the magnet before storage.
- Check the swivel joint and telescoping lock for drift or looseness.
- Replace cracked, deeply scratched, delaminated or heavily stained mirror heads.
- Store the tool in a sleeve, drawer slot or shadow board so the mirror face does not rub against cutting tools.
- If the tool has an LED, inspect the battery compartment for corrosion and keep spare batteries where permitted by shop policy.
A reasonable rule is simple: if the mirror cannot show a clean, stable image of a known surface under good lighting, it should not be used for acceptance-related inspection.
When to choose a different inspection method
A magnetic inspection mirror is not the right tool for every hidden feature. A borescope is better for deep internal cavities, long tubes, internal passages and areas where images need to be saved. A CMM, height gage, profilometer, thread gage or dedicated fixture is required when the question is dimensional conformance rather than visual condition. Dye penetrant, magnetic particle inspection, ultrasonic testing or radiography may be needed for certain discontinuities in welds or castings, depending on the governing specification.
Use the mirror when the task is visual access. Escalate to another method when the task requires measurement, permanent evidence, defect sizing, internal navigation, non-destructive testing or formal acceptance against a controlled specification. This distinction keeps the inspection mirror useful without overstating its capability.
Frequently asked questions
Is an inspection mirror with magnet a measuring tool?
Usually no. It is a visual aid. It may be part of an inspection process, but it does not normally provide traceable dimensional data. If a feature must be measured, use a suitable calibrated instrument or documented inspection method.
Can a magnetic inspection mirror be used inside a CNC machine?
Yes, but only under the shop’s safe operating procedure. The machine should be in a safe state before the mirror is placed near tools, spindles, chips, vises or fixtures. Chips on the magnet should be removed before the tool contacts finished or precision surfaces.
What mirror size is best for burr inspection?
A small flat mirror with strong angled light is usually better than a large convex mirror for burr inspection. The flat surface preserves detail, while side lighting helps reveal raised material by shadow.
Does the magnet affect inspection accuracy?
The magnet does not change the visual image, but it can affect the process if it attracts chips, pulls the mirror out of position or is placed near magnetically sensitive equipment. Cleanliness and placement matter.
When should the mirror be replaced?
Replace it when scratches, clouding, cracks, weak joints or unstable telescoping sections prevent a clear and repeatable view. For acceptance-related checks, image quality and stability are more important than tool cost.