Machinery manufacturing process explained for industrial equipment
What machinery manufacturing means in practice
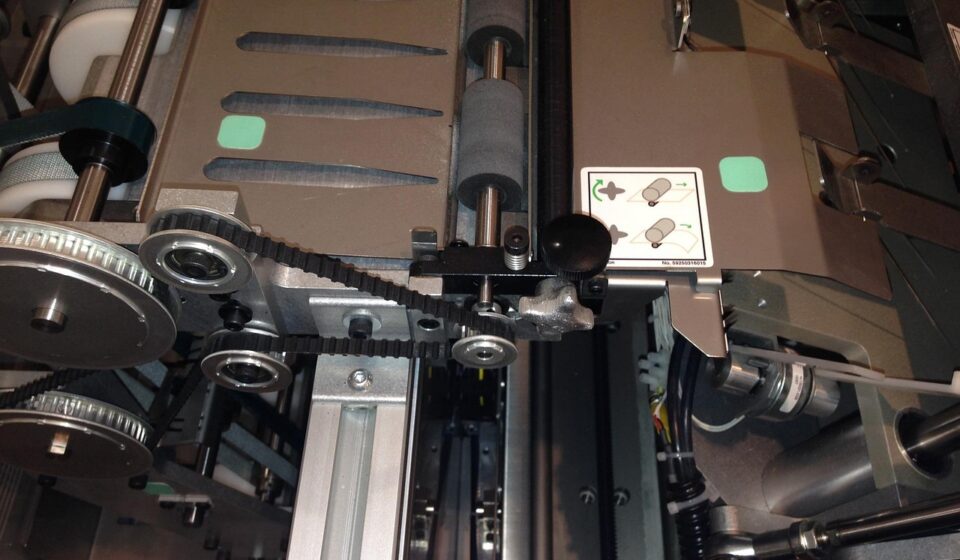
Machinery manufacturing is the controlled process of turning an equipment concept into a reliable industrial machine. It brings together engineering design, material selection, fabrication, machining, assembly, testing and documentation. For buyers, engineers and plant managers, the process is not simply about cutting metal or bolting parts together. Each decision affects cost, lead time, safety, maintainability and long-term performance.
In a typical project, the manufacturer converts performance requirements into drawings, tolerances, bills of materials, production routes and inspection plans. The same logic applies whether the final product is a packaging line, a hydraulic press, a CNC machine, a conveyor system or a custom automation cell. For more background on related production methods, see our manufacturing processes section.
The core stages of machinery manufacturing
Every machine has its own engineering requirements, but most machinery manufacturing projects follow a similar sequence. The order matters. A design issue found during review is usually far cheaper to correct than the same issue found during final assembly or factory testing.
| Stage | Main objective | Typical output |
|---|---|---|
| Requirement definition | Clarify function, capacity, environment and compliance needs | Specification, acceptance criteria, risk notes |
| Engineering design | Convert requirements into mechanical, electrical and control designs | Drawings, models, calculations, bill of materials |
| Process planning | Decide how parts and subassemblies will be produced | Routing, tooling plan, inspection plan |
| Fabrication and machining | Create frames, housings, shafts, plates and precision components | Finished parts ready for assembly |
| Assembly and integration | Build the machine and connect mechanical, electrical and control systems | Functional equipment or module |
| Testing and validation | Confirm performance, safety and quality requirements | Test records, corrective actions, release documents |
The first stage is requirement definition. A useful specification describes rated capacity, duty cycle, operating environment, available floor space, utilities, noise limits, safety expectations and maintenance access. Vague requirements can lead to oversized components, weak guarding, poor service access or controls that do not match the operator’s workflow.
Engineering design then turns those requirements into geometry and system architecture. Mechanical engineers define load paths, stiffness, bearing selection, lubrication points and service clearances. Electrical and controls engineers specify sensors, actuators, drives, control panels, interlocks and human-machine interfaces. In modern equipment projects, design review should cover more than whether the machine can run. It should also ask whether the machine can be built, inspected, maintained and upgraded.
Materials, machining and fabrication choices
Material selection is one of the earliest cost and performance decisions in machinery manufacturing. Carbon steel is widely used for frames and structural weldments because it is strong, available and cost-effective. Stainless steel is often selected where corrosion resistance, washdown requirements or hygiene expectations matter. Aluminum can be useful where lower weight, easier machining or corrosion resistance is important, although it may not suit every heavy-load structure.
Machined components such as shafts, bearing housings, gears, tooling plates and precision brackets require tighter control of dimensions and surface finish. Common methods include CNC milling, turning, drilling, grinding and electrical discharge machining for certain hard or complex features. The right method depends on tolerance, material hardness, production volume, feature complexity and inspection method.
Fabrication covers the cutting, bending, welding and forming operations used to create frames, guards, bases, tanks and sheet-metal enclosures. Welding quality is especially important because distortion can affect later machining and final alignment. A practical production plan often sequences rough fabrication, stress relief where needed, machining of critical surfaces and final finishing to reduce the risk of dimensional movement after assembly.
Additive manufacturing can also support machinery production, but it needs careful application. It is useful for prototypes, fixtures, lightweight brackets, complex ducts and low-volume components that are difficult to machine conventionally. For safety-critical or high-load parts, manufacturers still need material data, process qualification and inspection methods before treating printed components as direct replacements for forged, cast or machined parts.
Quality control is built into the process
Quality in machinery manufacturing is not a final inspection event. It is a system of controls applied throughout the project. ISO describes ISO 9001 as a quality management system standard that sets requirements for organizations seeking to meet customer and regulatory requirements and improve customer satisfaction. In machinery production, that principle translates into document control, supplier qualification, inspection planning, calibration, corrective actions and traceable records.
Dimensional inspection is central for precision equipment. Calipers, micrometers, height gauges, coordinate measuring machines, laser trackers and surface finish instruments may all be used, depending on the part and the tolerance involved. For welded or safety-related structures, inspection may also include visual checks, weld procedure controls and non-destructive examination when required by the application or customer specification.
Quality control should also cover purchased components. Motors, gearboxes, bearings, linear guides, sensors, pneumatic parts and hydraulic components can all affect final machine performance. A low-cost purchased part may increase downtime if it is difficult to source, poorly documented or incompatible with the control system. For this reason, manufacturers often balance price against availability, service life, documentation quality and technical support.
The most useful inspection plans are tied to risk. A cosmetic cover does not need the same control level as a spindle shaft, lifting component or safety interlock bracket. By ranking features according to function and failure consequence, teams can focus measurement time where it improves reliability instead of creating paperwork that does not reduce risk.
Safety, compliance and machine guarding
Safety is a design requirement, not an accessory added after the machine is complete. In the United States, OSHA’s general machine guarding rule states that guarding methods must protect operators and other employees from hazards such as point-of-operation risks, ingoing nip points, rotating parts, flying chips and sparks. For machinery manufacturers, this means guards, interlocks, emergency stops, safe access and warning information should be considered during design and validation.
Common machinery hazards include pinch points, stored energy, unexpected start-up, sharp edges, high temperatures, hydraulic pressure, pneumatic movement and electrical exposure. A safer design reduces reliance on operator behavior alone. Physical guarding, lockout provisions, control reliability, clear maintenance access and proper labeling all help reduce the chance that routine work becomes dangerous.
Compliance responsibilities vary by market and application. A machine intended for food processing, medical manufacturing, heavy construction, chemical handling or explosive atmospheres may face additional requirements beyond general industrial safety practice. Exported machinery may also need different documentation and conformity assessment depending on the destination market. Compliance should therefore be defined at the requirement stage, not discovered during shipment or installation.
How digital tools are changing machinery manufacturing
Digitalization has changed how machinery is designed, produced and supported. Computer-aided design, computer-aided manufacturing, simulation and product data management help teams find clashes, validate motion, manage revisions and generate manufacturing data. These tools do not replace engineering judgment, but they reduce the chance that production teams work from outdated drawings or incomplete design intent. See also: cnc and robotics.
NIST’s smart manufacturing work highlights areas such as real-time data analytics, predictive analytics, process control, prognostics, industrial control security and performance assurance. These themes matter because modern machinery increasingly includes sensors, software, networked controls and data feedback loops. A machine may now be evaluated not only by cycle time and accuracy, but also by the quality of the operational data it produces.
Digital twins and simulation can be valuable when equipment is complex, highly automated or expensive to modify after installation. A simulation may help test robot reach, conveyor accumulation, fixture access or maintenance clearance before steel is cut. However, digital models are only as good as their assumptions. Friction, vibration, operator behavior, part variation and supplier substitutions can still create differences between the model and the real machine.
For many manufacturers, the practical path is incremental. Start with controlled drawings and bills of materials, then connect inspection data, production scheduling, maintenance records and machine feedback. A fully connected factory is less useful if basic revision control, calibration and root-cause analysis are weak.
Cost, lead time and supply chain factors
The cost of industrial machinery is shaped by more than raw material and labor hours. Engineering time, purchased components, tooling, inspection, documentation, testing, packaging, shipping and installation support can all be significant. Custom machinery also carries uncertainty because design changes, supplier delays and integration issues can appear after the project has started.
Lead time is often driven by long-lead components such as castings, special motors, gearboxes, controls hardware, linear motion systems, hydraulic units and imported precision parts. In some projects, the best scheduling decision is to release stable long-lead items early while keeping flexible components open until the design is fully reviewed. That approach requires disciplined change control so early purchasing does not lock the team into a flawed design.
Design for manufacturability can reduce both cost and lead time. Examples include using standard material sizes, avoiding unnecessary tight tolerances, reducing unique fastener types, designing parts that can be inspected easily, and grouping similar machining operations. The goal is not to make the machine cheap at any cost. The goal is to spend money where it improves performance, safety or reliability.
Supply chain resilience has also become part of machinery planning. Manufacturers may evaluate whether critical components have approved alternates, whether software licenses are transferable, whether spare parts can be stocked locally and whether obsolete controls could create long-term service risk. These decisions affect the total cost of ownership long after the machine leaves the factory.
What to evaluate when comparing machinery manufacturers
When comparing machinery manufacturers, buyers should look beyond sales claims and focus on evidence. Useful signs include clear engineering documentation, structured design reviews, practical experience with similar duty cycles, transparent acceptance criteria, and a willingness to discuss risks before quoting a final price.
- Engineering capability: Can the team explain load calculations, tolerance choices, control architecture and maintenance access?
- Manufacturing depth: Does the company control critical machining, fabrication or assembly steps, or does it rely heavily on subcontractors?
- Quality records: Are inspection plans, calibration records, nonconformance handling and final test reports available?
- Safety approach: Are guarding, interlocks, emergency stops and service procedures designed into the machine from the beginning?
- Supportability: Are spare parts, drawings, manuals, software backups and troubleshooting information organized for long-term use?
The lowest purchase price is not always the lowest ownership cost. A machine that is difficult to maintain, slow to change over or dependent on unavailable parts can create far more cost through downtime than it saved at purchase. A stronger comparison considers productivity, reliability, safety, documentation and service life together.
Frequently asked questions
What is the difference between machinery manufacturing and general manufacturing?
General manufacturing can refer to the production of almost any goods, from consumer products to chemicals. Machinery manufacturing is more specific. It focuses on equipment, mechanical systems and industrial machines that often combine fabricated structures, precision components, electrical systems, controls and safety features.
Why are tolerances so important in machinery manufacturing?
Tolerances define the allowable variation in a part or assembly. If tolerances are too loose, the machine may vibrate, leak, wear quickly or fail to align. If tolerances are tighter than necessary, production costs rise without improving function. Good machinery design matches tolerance levels to the actual performance requirement.
How does automation affect machinery manufacturing?
Automation changes both the machines being built and the way they are produced. Manufacturers may use CNC equipment, robotic welding, automated inspection and digital work instructions. At the same time, many finished machines now include sensors, motion control, programmable logic controllers and data interfaces.
What documents are usually needed for an industrial machine?
Documentation often includes drawings, bills of materials, electrical schematics, pneumatic or hydraulic diagrams, operating manuals, maintenance instructions, spare parts lists, inspection records and test reports. Regulated or safety-critical applications may require additional compliance documents.
Conclusion
Machinery manufacturing combines engineering, process control, skilled production and risk management. Strong projects define requirements early, select materials and processes according to function, build quality checks into each stage, and treat safety as part of the design. Digital tools and smart manufacturing methods can improve visibility and performance, but they work best when basic engineering discipline is already in place. For industrial buyers and manufacturing teams, understanding the process makes it easier to control cost, reduce delays and specify machines that remain reliable in real production conditions.