Manufacturing processes explained for modern production planning
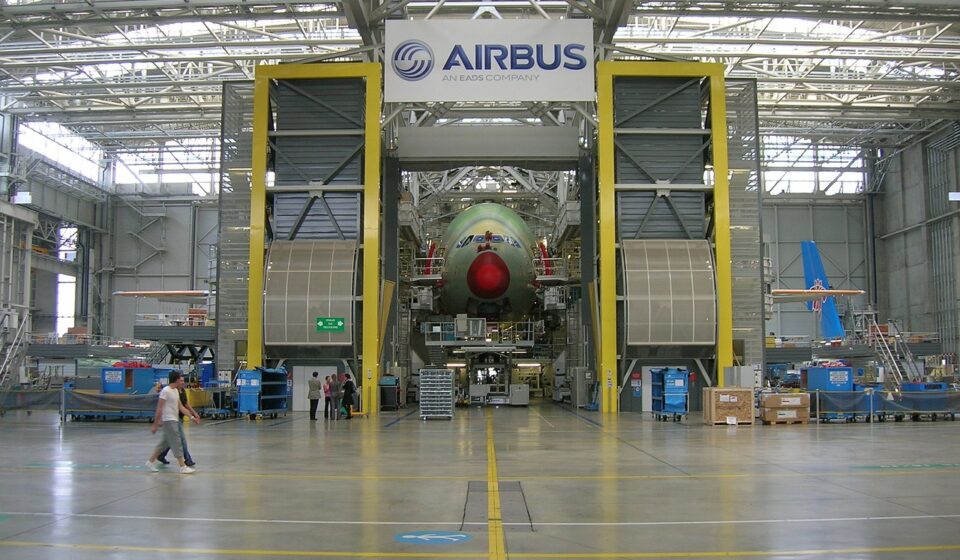
What manufacturing processes include
Manufacturing processes are the controlled steps used to convert materials into parts or finished products. They may change shape, dimensions, material properties, surface condition, or assembly state. For production planning, the question is not only which process can make a part, but which process can make it repeatedly at the required quality, cost, rate, and risk level.
A metal bracket, for example, may be stamped, machined, cast, forged, printed, or fabricated from welded pieces. Each route brings different tooling needs, tolerances, waste streams, inspection points, and lead times. This article explains the main process families, how they are selected, and how quality, safety, and digital controls affect shop-floor decisions. It draws on commonly used concepts from manufacturing engineering practice, NIST smart manufacturing work, ISO quality management guidance, OSHA machine-guarding rules, and ASME product-definition standards.
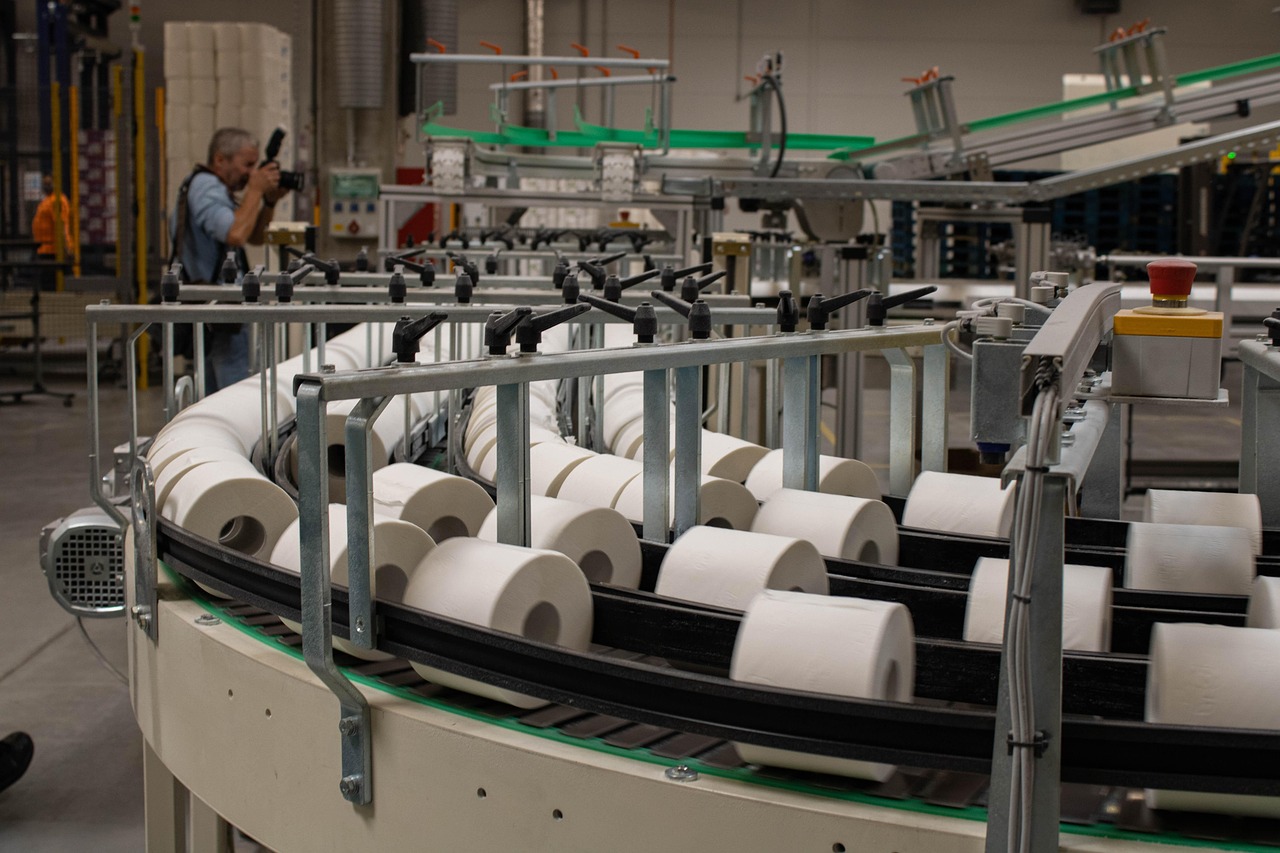
Main categories of manufacturing processes
Manufacturing processes are often grouped by the type of change they make to the material. In real factories, these categories overlap because most products move through several processes before they are complete. A die-cast housing may still need machining, surface finishing, inspection, and assembly. A printed metal component may still need heat treatment and post-machining. The categories are useful because they help engineers compare process capability before committing to tooling, equipment, or suppliers.
- Casting and molding. Material is shaped in a cavity or mold. Metal casting, plastic injection molding, die casting, sand casting, and compression molding are common examples. These processes can be efficient for complex shapes and medium-to-high volumes, but tooling design, shrinkage, porosity, cooling rate, and material flow must be controlled.
- Forming and deformation. Material is shaped by force without removing much material. Forging, rolling, extrusion, stamping, bending, and deep drawing are examples. Forming can deliver strong parts and high throughput, especially in metals, but it depends on ductility, tooling strength, springback control, lubrication, and press capacity.
- Machining and material removal. Cutting, milling, turning, drilling, grinding, electrical discharge machining, and abrasive waterjet cutting remove material to create geometry. Machining is valuable for tight tolerances, prototypes, repair work, and precision surfaces. Its limits often involve cycle time, tool wear, fixturing, chip handling, and material waste.
- Joining and assembly. Welding, brazing, soldering, riveting, fastening, press fitting, adhesive bonding, and mechanical assembly combine parts into a functional product. Joining decisions must consider strength, heat effects, corrosion, disassembly, inspection access, and field service needs.
- Additive manufacturing. Additive processes build parts layer by layer from polymers, metals, ceramics, or composites. They can reduce tooling needs and enable internal channels or complex lattice structures, but they also raise questions around build orientation, support removal, surface finish, anisotropy, qualification, and post-processing.
- Heat treatment and surface finishing. These processes change material properties or surface condition rather than the basic shape. Annealing, hardening, carburizing, anodizing, coating, polishing, shot peening, and plating can affect wear, corrosion resistance, fatigue life, friction, and appearance.
How to choose a manufacturing process
Process selection starts with the product requirement, not with the available machine list. The drawing, model, material specification, function, expected volume, and quality plan define the problem. A process that looks inexpensive for one prototype may become costly at production volume. Conversely, a high-tooling process may be uneconomical for ten parts but efficient for hundreds of thousands.
| Decision factor | Why it matters | Practical questions |
|---|---|---|
| Material | Material behavior determines formability, machinability, weldability, heat response, and defect risk. | Will the material crack, warp, work-harden, absorb moisture, oxidize, or require controlled atmosphere processing? |
| Geometry | Thin walls, undercuts, internal channels, deep holes, and sharp corners may favor or exclude certain routes. | Can the geometry be released from a tool, held in a fixture, machined with available tools, or inspected reliably? |
| Tolerance and surface finish | Nominal shape is not enough; fit, sealing, fatigue, noise, and assembly depend on allowable variation. | Which features need tight control, and can the process hold them without excessive scrap or rework? |
| Production volume | Volume changes the economics of tooling, automation, setup time, inspection strategy, and supplier choice. | Is the project closer to prototype, bridge production, batch manufacturing, or continuous high-volume output? |
| Quality and inspection | Some processes create hidden defects or variation that require special controls. | Can critical characteristics be measured in-process, at the end of the line, or through nondestructive testing? |
| Safety and compliance | Cutting, pressing, welding, molding, and chemical processes create different hazards and regulatory duties. | What guarding, ventilation, lockout, personal protection, and training are required? |
| Sustainability and waste | Energy use, scrap rate, coolant, emissions, and material recovery affect both cost and environmental impact. | Can near-net-shape processing, recycling, optimized nesting, or lower-temperature processing reduce waste? |
The most reliable decisions compare several routes against the same requirement set. A structured comparison may show that one process has the lowest piece price, another has the shortest lead time, and a third has the lowest technical risk. The selected route should reflect the project constraint that matters most.
From design intent to shop-floor control
Product definition and tolerances
Process planning depends on clear product definition. Dimensions, datums, tolerances, material callouts, surface finish notes, and inspection requirements must show what is functionally important. ASME Y14 standards, including dimensioning and tolerancing practices used in mechanical design, are widely used to reduce ambiguity between design, manufacturing, and inspection teams. Geometric dimensioning and tolerancing is not a manufacturing process, but it strongly influences which process can meet a requirement at an acceptable cost.
Routing, tooling and parameters
Once the requirement is defined, planners determine the routing: the sequence of operations, machines, tools, fixtures, programs, heat treatments, cleaning steps, inspections, and packaging. A simple routing decision can change the result. Machining a thin-walled part before stress relief may produce distortion. Welding before machining may simplify assembly but add residual stress. Forming before piercing may improve edge quality in one case and complicate die design in another.
Control parameters are just as important. Feed rate, cutting speed, mold temperature, injection pressure, furnace cycle, weld current, clamping force, tool offset, and coolant condition are not minor settings; they are part of the process definition. When those parameters drift, quality can drift even if the equipment and material remain the same.
Inspection loops
Inspection should be built into the process, not treated only as final sorting. Incoming material checks, first-article inspection, in-process gauging, statistical process control, nondestructive testing, and final verification serve different purposes. Final inspection can detect nonconforming parts, but in-process control is usually better at preventing them. The goal is to identify where variation enters the process and control it before it becomes scrap, rework, or field failure.
Quality, safety and sustainability considerations
Quality as a process system
ISO quality management guidance emphasizes a process approach: organizations should understand processes, their sequence, and their interaction rather than manage activities as isolated tasks. In manufacturing, this means a defect may not originate where it is discovered. Poor surface finish after machining may trace back to casting hardness variation, fixture movement, tool wear, coolant concentration, or an unclear tolerance requirement. A process-based view supports root-cause analysis across the chain.
Machine safety at the point of operation
Safety requirements are not optional additions to process selection. In the United States, OSHA machine-guarding rules for general industry require guarding methods to protect operators and nearby employees from hazards such as point-of-operation exposure, ingoing nip points, rotating parts, flying chips, and sparks. The exact control depends on the machine and task, but safety must be considered during layout, tooling, maintenance access, automation design, and work instruction development.
Sustainability and resource use
Manufacturing sustainability is practical, not abstract. Energy intensity, yield, scrap handling, coolant management, compressed-air losses, heat recovery, powder reuse, tool life, and packaging can materially affect production cost and environmental performance. NIST smart manufacturing work has highlighted the importance of measuring energy and material performance along with traditional cost, quality, reliability, and productivity metrics. That broader measurement view helps teams see trade-offs that a piece-price comparison may miss.
Smart manufacturing and process data
Modern manufacturing processes increasingly rely on data from sensors, controllers, inspection equipment, manufacturing execution systems, and production software. NIST describes smart manufacturing implementations as using information technology, sensor networks, computerized controls, and production management software to improve performance. In practice, this can mean monitoring spindle load to predict tool wear, tracking furnace temperature uniformity, using vision systems for assembly verification, or connecting inspection data back to machine offsets.
Digital tools can improve process control, but they do not replace process knowledge. A dashboard cannot fix an unstable fixture, a vague drawing, a poor datum scheme, or an unrealistic tolerance. Data is most useful when it is tied to known process inputs, defined quality characteristics, and clear reaction plans. If a control chart signals drift, the team must know who responds, what is adjusted, and when production is stopped.
Smart manufacturing also has limits. Data quality, cybersecurity, equipment compatibility, operator training, and legacy machine integration can slow adoption. The practical path is often incremental: start with a critical process, define the failure modes, measure the most useful variables, and connect the data to a decision.
A practical checklist for comparing process routes
- Define the function. Identify which surfaces, dimensions, materials, and properties affect performance, not just appearance.
- Separate must-have requirements from preferences. Tight tolerances, special finishes, and exotic materials should be justified by function.
- Compare at least two routes. Include tooling cost, setup time, cycle time, scrap, inspection, post-processing, logistics, and changeover risk.
- Check process capability early. A process should demonstrate that it can hold critical characteristics, not merely produce one acceptable sample.
- Review safety and maintenance access. Guarding, ventilation, lockout points, ergonomics, and cleaning procedures should be part of the process concept.
- Plan inspection before launch. Decide where to measure, how often to measure, what equipment is needed, and what action follows an out-of-control signal.
- Consider lifecycle changes. Prototype, ramp-up, mature production, and end-of-life service may each require different process priorities.
This checklist is most useful when design, manufacturing, quality, purchasing, and safety teams use it together. A process route chosen only by engineering may overlook supplier capacity. A route chosen only by purchasing may overlook inspection difficulty. A route chosen only for speed may create rework that delays launch.
Frequently asked questions
What is the difference between a manufacturing process and a production system?
A manufacturing process is a specific method for changing material or assembling parts, such as milling, casting, welding, molding, or heat treatment. A production system is the wider arrangement of people, machines, information, material flow, quality controls, maintenance, and scheduling that uses those processes to deliver products.
Which manufacturing process gives the tightest tolerances?
There is no universal answer. Precision grinding, high-quality machining, honing, lapping, and some EDM operations can achieve tight tolerances, but the result depends on material, geometry, machine condition, fixturing, thermal stability, measurement method, and operator or automation control. The right question is whether a process can repeatedly hold the specified tolerance for the chosen part.
When is additive manufacturing a practical choice?
Additive manufacturing is often practical for prototypes, low-volume complex parts, lightweight structures, internal channels, customized products, tooling inserts, and spare parts where traditional tooling is slow or expensive. It may be less suitable when high production speed, very smooth as-built surfaces, low material cost, or established qualification routes are the main priorities.
Why do manufacturing processes often need post-processing?
Primary processes create the main shape, but they may not deliver final properties or surfaces. Castings may need machining, heat treatment, and cleaning. Weldments may need stress relief or inspection. Printed metal parts may need support removal, heat treatment, machining, and surface finishing. Post-processing should be included in cost and lead-time estimates from the beginning.
How should small manufacturers start improving process control?
Start with one process that causes repeat scrap, rework, downtime, or customer complaints. Define the critical characteristic, document the current method, measure the key input variables, verify the inspection method, and create a reaction plan. Small, disciplined control steps often produce more value than collecting large amounts of unused data.
For more manufacturing context and process explainers, visit Poduai.com.