Production processes in manufacturing explained for practical factory planning
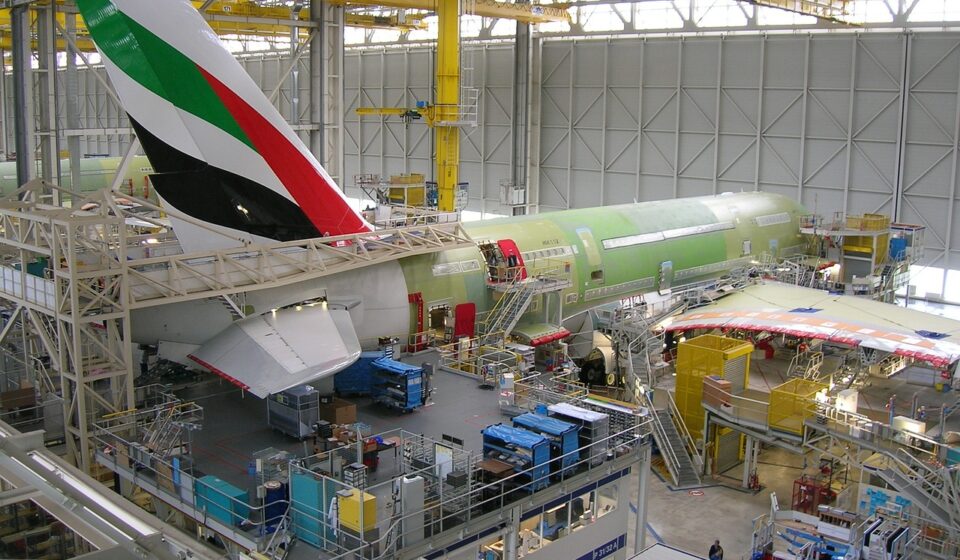
What production processes in manufacturing mean
Production processes in manufacturing are the technical methods and organized workflows used to transform raw materials, components, or substances into finished goods. For factory planning, the term goes beyond a single machine operation. It covers how a part is formed, cut, joined, treated, inspected, moved, scheduled, and controlled until it meets product requirements.
The right process route depends on material behavior, geometry, tolerance, demand volume, cost targets, quality risk, labor skill, equipment capability, and delivery expectations. The question is not only whether a process can make the part. It is whether it can make the part repeatedly, safely, economically, and at the required quality level. That is why a clear understanding of manufacturing processes matters in product design, plant layout, capacity planning, quality management, and continuous improvement.
Public industrial classifications such as NAICS describe manufacturing as the mechanical, physical, or chemical transformation of materials or components into new products. Quality management standards also emphasize the process approach, where activities are planned, controlled, measured, and improved as connected systems rather than isolated tasks.
Main families of production processes
Manufacturing processes can be grouped in several ways. For production planning, it is useful to classify them by how they change the material or product. Most industrial products use a sequence of process families rather than one standalone method.
| Process family | What it does | Common examples | Typical planning concern |
|---|---|---|---|
| Primary shaping | Creates the basic form of a part | Casting, molding, forging, extrusion, powder metallurgy, additive manufacturing | Tooling cost, material flow, shrinkage, cycle time, defect risk |
| Material removal | Removes material to reach shape, tolerance, or finish | Milling, turning, drilling, grinding, laser cutting, waterjet cutting | Accuracy, tool wear, setup time, chip control, machine utilization |
| Joining and assembly | Combines parts into a subassembly or final product | Welding, brazing, soldering, fastening, adhesive bonding, press fitting | Joint strength, distortion, sequence, fixturing, rework access |
| Heat, chemical, and surface treatment | Changes material properties or surface performance | Heat treating, anodizing, plating, coating, passivation, carburizing | Batch control, contamination, environmental controls, traceability |
| Finishing and inspection | Verifies and prepares the product for use or shipment | Deburring, polishing, cleaning, visual inspection, dimensional inspection, functional testing | Measurement method, acceptance criteria, bottlenecks, documentation |
Additive manufacturing is often discussed separately because it builds geometry layer by layer rather than removing material from stock or using a fixed mold. Standard terminology in the ISO/ASTM 52900 series commonly groups additive manufacturing into seven process categories: powder bed fusion, material extrusion, binder jetting, directed energy deposition, material jetting, sheet lamination, and vat photopolymerization. In production, additive methods may reduce tooling needs and enable complex geometry, but they still require process validation, post-processing, inspection, and material control.
Flow types shape factory economics
The technical process is only one part of the production decision. The flow type determines how work moves through the factory, how inventory builds up, how labor is organized, and how quickly the system can respond when demand changes.
| Flow type | Best suited for | Strengths | Limitations |
|---|---|---|---|
| Job shop | Low-volume, high-variety work | Flexible equipment, skilled labor, custom routing | Complex scheduling, longer lead times, higher setup burden |
| Batch production | Repeated products made in groups | Balances variety and efficiency, supports shared equipment | Changeovers, queue time, batch quality issues |
| Cellular manufacturing | Part families with similar process routes | Shorter travel distance, clearer ownership, smoother flow | Requires good product grouping and capacity balance |
| Assembly line | High-volume products with stable sequence | High throughput, standardized work, easier takt planning | Less flexible, sensitive to line imbalance and stoppages |
| Continuous production | High-volume process industries | Very high utilization, consistent output, automated control | High capital cost, difficult shutdowns, strict process stability needs |
A precision machine shop making prototypes may use job shop routing because each order can have a different sequence. A plastic parts plant may use batch molding when tools and materials change during the week. A beverage, chemical, paper, or steel operation may rely on continuous production because stopping and starting the process is expensive. The correct flow type should match product variety, order pattern, equipment cost, labor model, and risk tolerance.
How manufacturers select the right process route
Process selection starts with product requirements. A design team may define the target material, dimensions, surface finish, strength, corrosion resistance, appearance, life cycle conditions, and regulatory or customer requirements. Process engineers then translate those requirements into a route that the factory can execute consistently.
Material and geometry
Materials respond differently to heat, pressure, cutting, forming, and chemical exposure. Aluminum, stainless steel, engineering plastics, ceramics, composites, and elastomers each narrow or expand the available process choices. Geometry also matters. Thin walls, internal channels, undercuts, deep holes, and tight radii may favor one method while making another impractical or too expensive.
Volume and variety
Low-volume work can justify flexible methods with limited tooling, even if unit cost is higher. High-volume work often justifies dedicated tooling, automation, fixtures, and line balancing because setup cost can be spread across many units. A process that is economical for 50 parts may be unsuitable for 500,000 parts. A process designed for 500,000 parts may be too rigid for frequent engineering changes.
Tolerances and quality risk
Near-net-shape processes such as casting, forging, or molding may create the main geometry efficiently, but precision surfaces may still need machining or grinding. Welding may be strong and fast, but it can introduce distortion or heat-affected zones. Coating may improve wear or corrosion resistance, but it can add thickness variation. A robust process route anticipates these effects instead of treating inspection as the only quality safeguard.
Tooling, changeover, and capacity
Tooling cost, fixture design, setup time, and changeover discipline often determine the real economics of production. A bottleneck machine can limit the output of an entire line. A process with a slightly longer cycle time may still be preferable if it reduces scrap, inspection burden, or downstream rework. Selection should compare total process performance, not only the visible cost of one operation.
From design to a production process plan
A process plan converts design intent into manufacturing instructions. It normally includes the bill of materials, process sequence, equipment requirements, tooling, inspection points, work instructions, labor skills, setup data, packaging requirements, and routing information for planning systems.
A practical planning sequence often includes these steps:
- Review design requirements. Confirm material, dimensions, critical features, performance requirements, cosmetic expectations, and customer specifications.
- Assess manufacturability. Identify features that may drive cost, defects, difficult tooling, long cycle times, or unstable inspection results.
- Choose the process route. Define the order of shaping, machining, treatment, assembly, inspection, and packaging steps.
- Define resources. Assign machines, tools, fixtures, gauges, operators, maintenance needs, and material handling methods.
- Control risk. Use methods such as process failure mode and effects analysis, control plans, first article inspection, and pilot runs where appropriate.
- Release and improve. Document work standards, collect production data, and update the process when defects, delays, or design changes reveal better options.
NIST manufacturing reference models describe production process definition as a bridge between product design data and factory execution, including required capabilities, sequencing, routing, cost estimates, and manufacturing data packages. In simpler terms, process planning is where the product idea becomes a repeatable shop-floor method. See also: cnc and robotics.
Key metrics and control points
A production process is only useful if it can be controlled. Manufacturers typically monitor a mix of quality, speed, cost, safety, and reliability metrics. The right metric depends on the process type, but several measures appear across many factories.
- First pass yield: the percentage of units that meet requirements without rework.
- Scrap and rework rate: the amount of material, labor, or product lost because the process did not meet requirements.
- Cycle time: the time required to complete a unit or operation.
- Throughput: the output rate of a process, line, or plant over a defined period.
- Overall equipment effectiveness: a common equipment performance measure that combines availability, performance, and quality.
- Changeover time: the time required to switch from one product, tool, material, or setup to another.
- Process capability: the ability of a process to stay within specification limits when it is stable and properly measured.
Control points should be placed where they prevent defects, not only where they detect finished failures. Controlling melt temperature in molding, weld parameters in joining, tool offsets in machining, or bath chemistry in surface treatment can reduce variation before it reaches final inspection. In regulated or high-reliability industries, traceability, calibration, operator qualification, and documented acceptance criteria become part of the production process itself.
How digital tools are changing process planning
Digital manufacturing does not remove the need for sound process engineering. It changes how quickly data can be captured, compared, and used. Sensors, machine connectivity, manufacturing execution systems, digital work instructions, simulation, and in-process measurement can help teams understand variation earlier than traditional end-of-line inspection alone.
NIST has described smart manufacturing in terms of integrated systems that can monitor, control, and optimize factory performance. In practice, this may mean using machine data to detect tool wear, production dashboards to expose bottlenecks, digital twins to test layout or scheduling options, and automated inspection to shorten feedback loops. These tools are valuable when the underlying process model is clear. If the route, specifications, or responsibilities are poorly defined, software often makes confusion more visible rather than solving it.
The strongest results usually come from combining process knowledge with disciplined data use. A factory should first understand which variables matter, how they are measured, who owns them, and what action follows when limits are exceeded. Technology then becomes a support system for better decisions, not a substitute for process control.
Common mistakes in production process design
Several recurring mistakes increase cost and risk during industrialization. One is choosing a process because it can make a sample, without proving that it can make stable production quantities. Another is designing parts without considering tooling access, inspection access, or assembly sequence. A third is assuming that final inspection can compensate for unstable inputs.
Manufacturers also underestimate hidden interfaces. A machining operation may depend on casting consistency. A coating process may depend on cleaning quality. An assembly line may depend on supplier packaging and part orientation. When these connections are ignored, problems show up as random defects, missed schedules, or excess inventory. Good process planning treats the production route as an interdependent system.
Frequently asked questions
What is the difference between a manufacturing process and a production process?
A manufacturing process usually refers to a technical method such as casting, machining, welding, molding, or coating. A production process is often broader. It includes the technical method plus routing, scheduling, inspection, labor, material handling, documentation, and control activities needed to make the product repeatedly.
Which production process is best for high-volume manufacturing?
High-volume manufacturing often favors assembly lines, dedicated tooling, automated cells, or continuous processes, depending on the product. The best choice depends on demand stability, product design, material, tolerance, capital budget, and changeover frequency. A high-volume process should be evaluated by total cost, quality stability, capacity, and flexibility.
Why does process routing matter?
Routing defines the order of operations and the resources used at each step. Poor routing can create long travel distances, bottlenecks, rework loops, excess work-in-process inventory, and unclear responsibility. Good routing supports predictable lead time, simpler scheduling, and better quality control.
Does additive manufacturing replace traditional production processes?
Additive manufacturing can replace some tooling-intensive or geometry-limited methods, especially for complex, low-volume, customized, or lightweight parts. It does not replace all traditional processes. Many additive parts still require heat treatment, machining, surface finishing, inspection, or assembly before they are ready for use.
How can a manufacturer improve an existing production process?
Improvement should start with measured evidence. Teams can map the current route, identify bottlenecks, measure defects and downtime, separate common causes from special causes, and test changes on the highest-impact variables. Durable improvements usually combine clearer standards, better control points, operator feedback, maintenance discipline, and design-for-manufacturing updates.